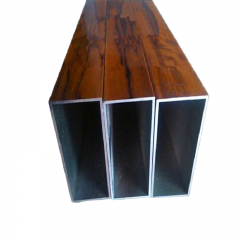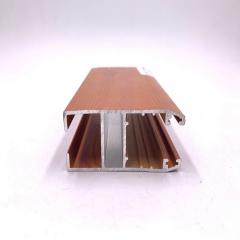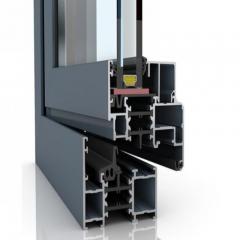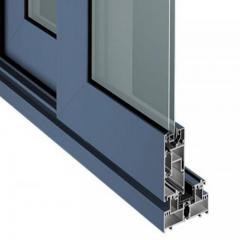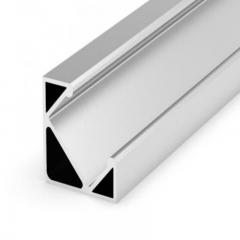
Ever wondered how those sleek aluminum window frames or sturdy industrial machine components get their precise shapes? The answer lies in a fascinating manufacturing technique that has revolutionized modern design and construction.
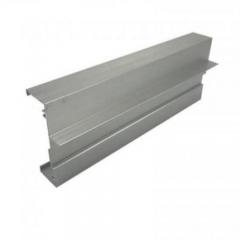
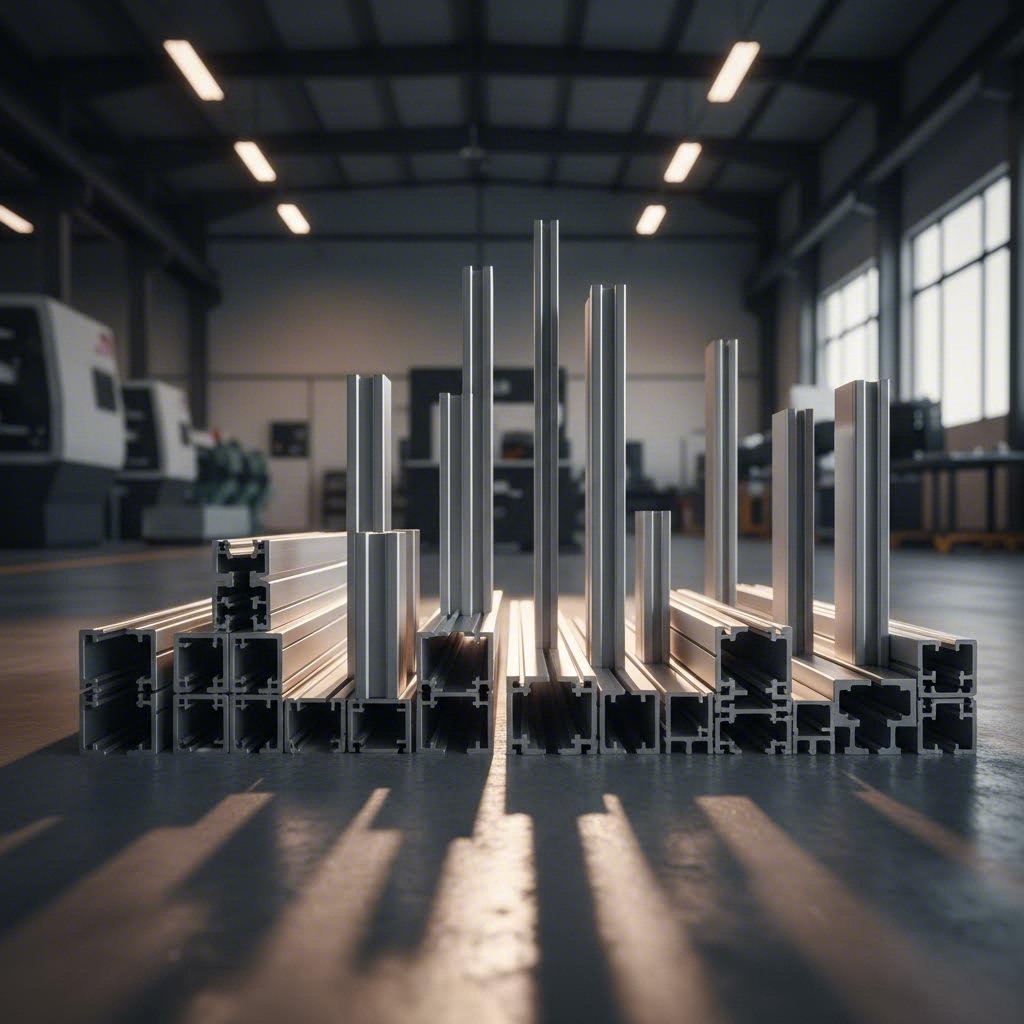
Aluminum extrusion profiles are continuous lengths of aluminum alloy shaped by forcing heated metal through a custom-designed steel die, creating parts with consistent cross-sections that can range from simple angles to complex architectural systems.
Think of it like squeezing toothpaste from a tube. The paste emerges in the exact shape of the tube's opening. In aluminum extrusion, a powerful hydraulic ram applies up to 15,000 tons of pressure to push softened aluminum through precisely engineered openings, producing everything from basic rectangular tubes to intricate multi-channel profiles.
The journey from raw material to finished profile involves carefully controlled steps. First, manufacturers preheat the steel die to approximately 750-900°F to ensure optimal metal flow and extend the die's lifespan. Simultaneously, they heat a cylindrical aluminum billet to 800-925°F, making it malleable without melting it completely.
Here's where the magic happens. After lubricating both the billet and the ram to prevent sticking, the hydraulic press forces the softened aluminum through the die opening. The metal emerges on the other side in a fully-formed shape, ready for cooling and further processing.
Once the extruded aluminum exits the press, it undergoes rapid cooling through water baths or air systems. This "quenching" process controls the material's mechanical properties. Workers then stretch the profiles to correct any twisting or deformation before cutting them to final lengths, typically between 8 and 24 feet.
Why does this manufacturing method matter so much? Three key advantages set extruded aluminum apart:
Unlike aluminum plate or a standard 4x8 aluminum sheet produced through rolling, extruded profiles offer virtually unlimited geometric possibilities. And compared to cast aluminum, which pours molten metal into molds, extrusion delivers superior tensile strength because the process creates a more organized grain structure. This distinction makes extruded aluminum the preferred choice when strength-to-weight ratio and dimensional consistency truly matter.
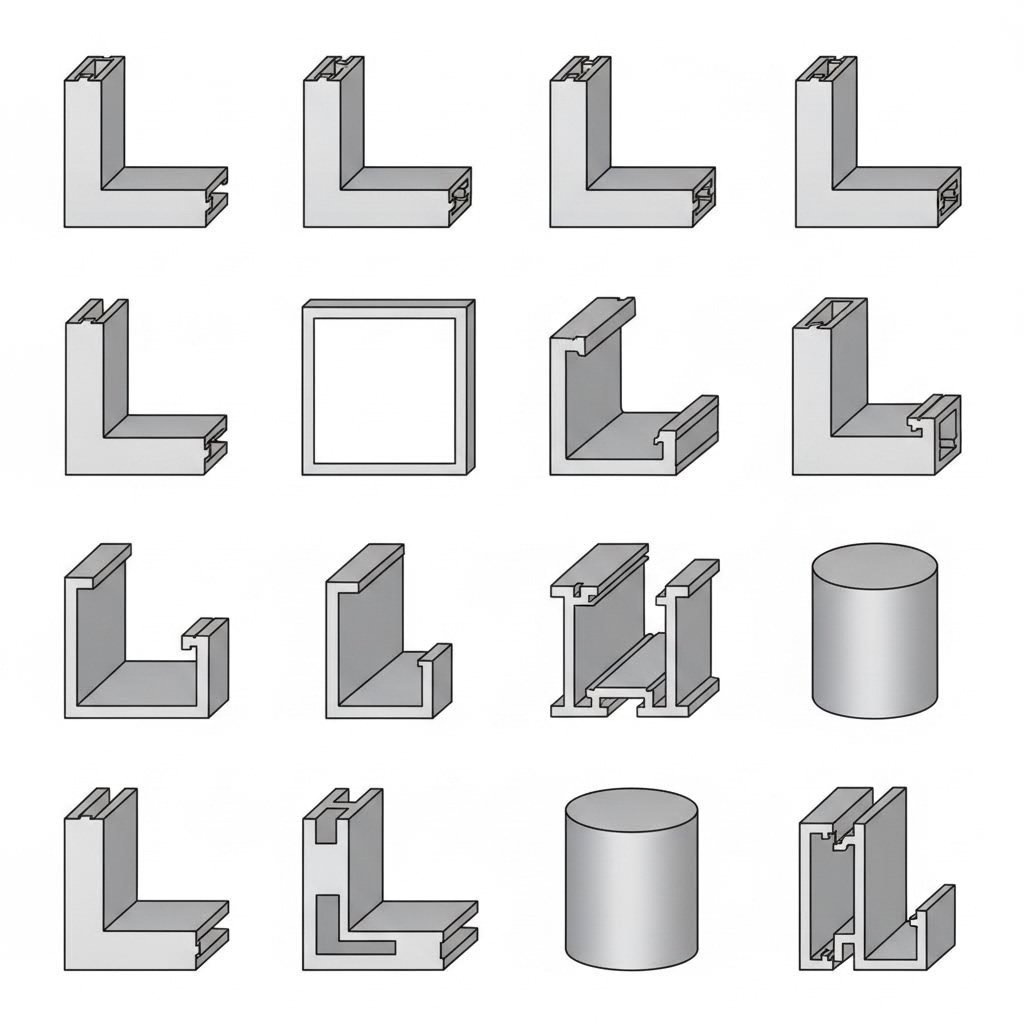
With so many aluminum extrusion shapes available, how do you know which one fits your project? Whether you're building a machine frame, designing architectural features, or creating custom enclosures, understanding the full spectrum of profile types helps you make smarter decisions. Let's break down the complete taxonomy that most aluminum shapes catalogs fail to explain clearly.
Standard shapes form the backbone of most aluminum extrusion applications. These profiles follow industry-standard dimensions, making them readily available and cost-effective for countless projects. Here's what you'll find in any comprehensive extruded shapes collection:
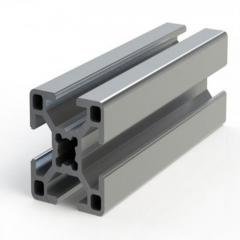
Here's where aluminum profiles get really interesting. T-slot framing systems represent a completely different design philosophy from standard shapes. Instead of permanent connections through welding or bolting, T-slot profiles feature continuous grooves that accept specialized hardware for tool-free assembly and reconfiguration.
Imagine building with adult-sized construction blocks. That's essentially what T-slot systems offer. The slots running along each face accept T-nuts, brackets, and connectors that slide into position and lock firmly in place. This modular approach transforms how engineers design workstations, machine guards, conveyor systems, and countless industrial applications.
What makes T-slot fundamentally different? Three key capabilities set these profiles apart:
Beyond standard shapes and T-slot systems, specialty profiles address specific industry needs. Heatsink profiles feature fins or ribs designed to dissipate thermal energy. Architectural mullions create the framework for curtain wall systems. LED housing profiles provide mounting channels with integrated diffuser options.
Understanding the structural classification of these aluminum profiles helps clarify their manufacturing complexity and cost implications:
| Profile Classification | Description | Common Examples | Relative Die Cost |
|---|---|---|---|
| Solid | No enclosed voids; continuous cross-section | Flat bars, angles, round rods, hex bars | Lowest |
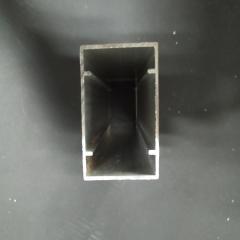
| Hollow | Completely enclosed void space | Round tubes, square tubes, rectangular tubes | Moderate to High |
| Semi-Hollow | Partially enclosed spaces with narrow openings | C-channels with tight gaps, some T-slot profiles | Moderate |
According to industry specifications, hollow shapes completely enclose a void within their cross-section, requiring more complex die designs with internal mandrels. Semi-hollow profiles feature partially enclosed spaces, like an extremely tight channel opening. This classification directly affects tooling costs, extrusion speeds, and ultimately your per-foot pricing.
When browsing an aluminum shapes catalog, you'll notice most suppliers organize offerings by these categories. Knowing whether your application requires solid structural support or hollow weight savings helps narrow options quickly before diving into specific dimensions and alloy grades.
You've selected the perfect profile shape for your project. Now comes an equally critical decision: which aluminum alloy grade delivers the performance you need? Many suppliers list alloy options without explaining why they matter. Let's change that by diving into the types of extruded aluminum that dominate the industry and what makes each one unique.
Often called "architectural aluminum," 6063 is the most popular aluminum alloy for extrusions. Why does it hold this top position? The answer lies in its exceptional extrudability and beautiful surface finish.
This alloy contains magnesium (0.45-0.9%) and silicon (0.2-0.6%) as its primary alloying elements. These lower concentrations compared to other 6000-series alloys allow the metal to flow smoothly through complex die shapes, producing crisp edges and smooth surfaces. When you see anodized aluminum window frames with that clean, professional appearance, you're almost certainly looking at 6063.
What makes 6063 shine in architectural applications?
When your aluminum extrusion profile needs to carry serious loads, 6061 steps up as the go-to choice. Known as "structural aluminum," this alloy delivers a better strength-to-weight ratio than 6063, making it ideal for demanding industrial and mechanical applications.
The difference comes from chemistry. 6061 contains higher concentrations of magnesium (0.8-1.2%) and silicon (0.4-0.8%), which boost its tensile strength significantly after heat treatment. You'll find extruded aluminum profiles in 6061 alloy throughout aerospace components, marine hardware, and heavy-duty machine frames.
Consider 6061 when your application demands:
You'll notice alloys listed with suffixes like T5 or T6. These temper designations indicate the heat treatment applied after extrusion, directly affecting mechanical properties.
Here's what happens during tempering: The aluminum is heated to approximately 980°F to dissolve alloying elements into a solid solution, then quenched in water. Subsequent aging at 325-400°F causes these elements to form ordered arrays within the aluminum matrix, significantly strengthening the material.
The practical difference? T5 temper results from cooling and aging directly from the extrusion process, while T6 temper involves a separate solution heat treatment before aging. T6 consistently delivers higher strength values, though at increased processing cost.
| Property | 6063-T5 | 6063-T6 | 6061-T6 | 7075-T6 |
|---|---|---|---|---|
| Tensile Strength (ksi) | 22 | 30 | 42 | 83 |
| Yield Strength (ksi) | 16 | 25 | 35 | 73 |
| Corrosion Resistance | Excellent | Excellent | Good | Fair |
| Weldability | Good | Good | Good | Poor |
| Machinability | Fair | Fair | Good | Good |
| Anodizing Response | Excellent | Excellent | Good | Fair |
| Relative Cost | Low | Low-Medium | Medium | High |
So when does standard aluminum like 6063-T5 make sense versus upgrading to 6061-T6 or specialty alloys? Consider these decision factors:
Choose 6063-T5 when: Surface appearance matters most, the profile will be anodized or powder coated, structural loads are moderate, and cost optimization is important. Window frames, door systems, and architectural trim are classic applications.
Choose 6061-T6 when: Strength requirements exceed 6063 capabilities, the profile undergoes significant machining, or the application involves higher stress levels. Machine frames, transportation components, and structural members benefit from this aluminium extrusion alloy.
Consider 6005 when: You need strength between 6063 and 6061 with better extrudability than 6061. This alloy works well for tubing, rail profiles, and applications requiring more strength than 6063 without the full jump to 6061.
Specify 7075 when: Maximum strength justifies premium pricing. As the strongest commercially available aluminum alloy, 7075 suits aerospace and highly stressed structural parts. However, its poor weldability and lower corrosion resistance require careful consideration.
The bottom line? Match the alloy to your actual requirements rather than defaulting to the strongest option. An aluminum extrusion profile in 6063-T5 costs less and performs beautifully for most architectural work, while 6061-T6 earns its place where structural demands justify the investment. Understanding these trade-offs ensures you're not overpaying for unnecessary performance or underspecifying for critical applications.
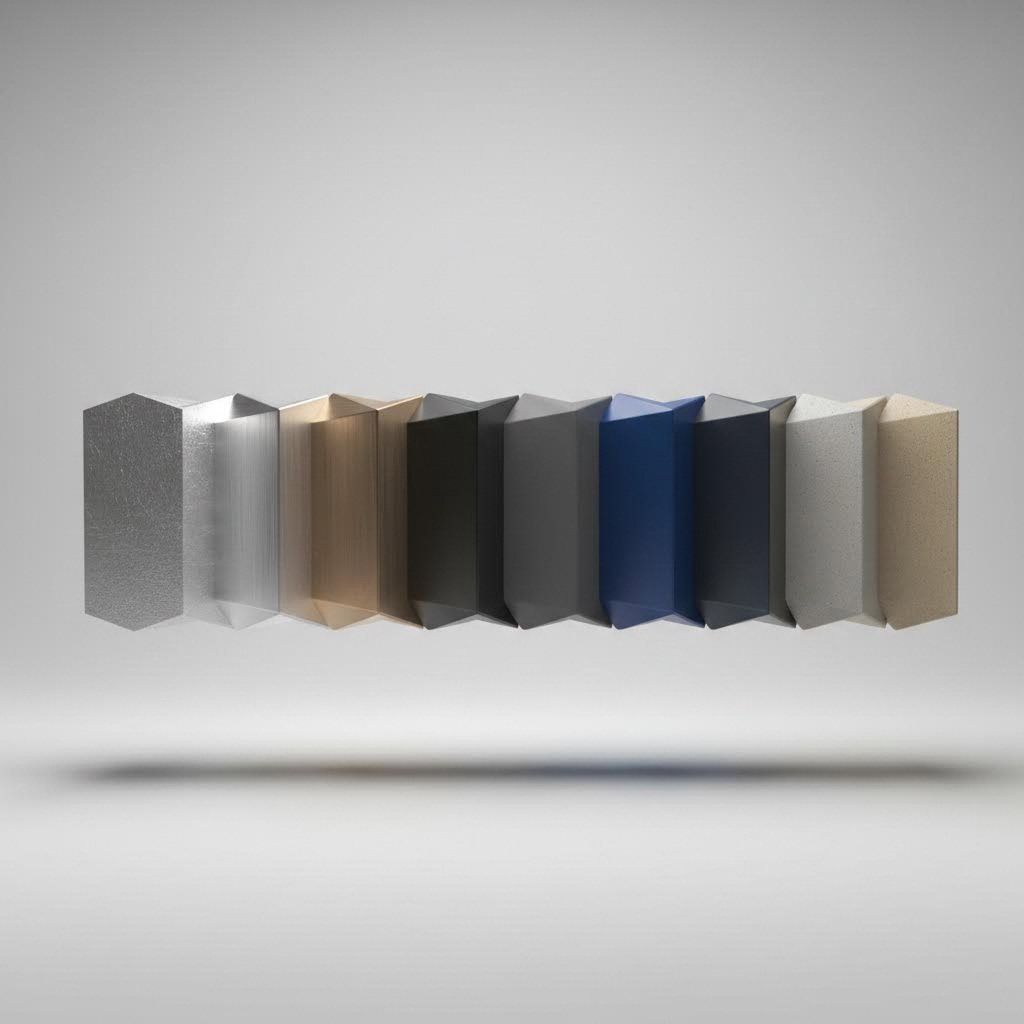
You've selected the right alloy grade for your aluminium profile. But here's a question many buyers overlook until it's too late: what surface finish will protect your investment and deliver the appearance you need? The finish you choose directly impacts durability, maintenance requirements, and visual appeal for years to come.
Unlike a simple coat of paint, aluminum surface treatments create permanent transformations that become integral to the metal itself. Let's explore the major finishing categories so you can match the right treatment to your specific application.
Anodizing isn't just applying a coating. It's an electrochemical process that transforms the aluminum surface into a protective oxide layer that becomes part of the base metal. This means it can't peel, chip, or flake like conventional paint. The result? A finish that's as hard as sapphire and remarkably resistant to corrosion and wear.
Three main types of anodizing serve different performance needs:
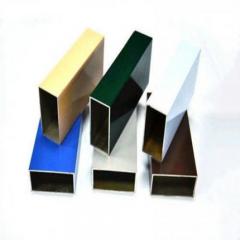
What about color options? Here's where anodizing gets interesting. The porous oxide layer accepts dyes before being sealed, creating permanent coloration within the finish itself. Popular anodized colors include:
Coating thickness directly affects longevity. According to industry experts, Class I anodizing (0.7 mils minimum) lasts approximately twice as long as Class II (0.4 mils) in exterior applications. For aluminum trim profiles exposed to weather, specifying adequate thickness protects your investment for decades rather than just years.
When unlimited color selection matters as much as protection, powder coating delivers what anodizing cannot. This process applies dry paint particles electrostatically to the profile aluminum surface, then cures them in an oven to create a tough, uniform finish.
Why choose powder coating over liquid paint? The advantages stack up quickly:
Powder coatings come in various resin formulations. Polyester TGIC powders offer good weatherability and are available in hundreds of stock colors. For applications demanding the highest performance, PVDF-based powders now meet stringent AAMA 2605 specifications previously achievable only with liquid coatings.
Some applications push beyond what standard anodizing or powder coating can handle. That's where specialty finishes earn their premium pricing.
PVDF Coatings (Kynar/Hylar)
For architectural aluminum extrude applications requiring exceptional weathering performance, PVDF coatings set the industry standard. These 70% polyvinylidene difluoride formulations have dominated curtain wall and metal roofing markets since 1965.
What makes PVDF special? The carbon-fluorine bonds in the resin are among the strongest chemical bonds available, providing stubborn resistance to chalking, fading, and airborne pollutants. Buildings coated with quality PVDF finishes maintain their appearance for 30+ years with minimal maintenance.
Mill Finish Applications
Not every profile aluminum application requires a protective finish. Mill finish, the natural surface condition after extrusion, works perfectly in situations where:
How do you choose? Consider these factors when specifying surface treatments for your aluminum extruded profiles:
The finish you select becomes a permanent part of your aluminium profile investment. Getting it right the first time prevents costly refinishing or premature replacement. When in doubt, consult with your extrusion supplier about which treatments best match your specific application conditions and performance expectations.
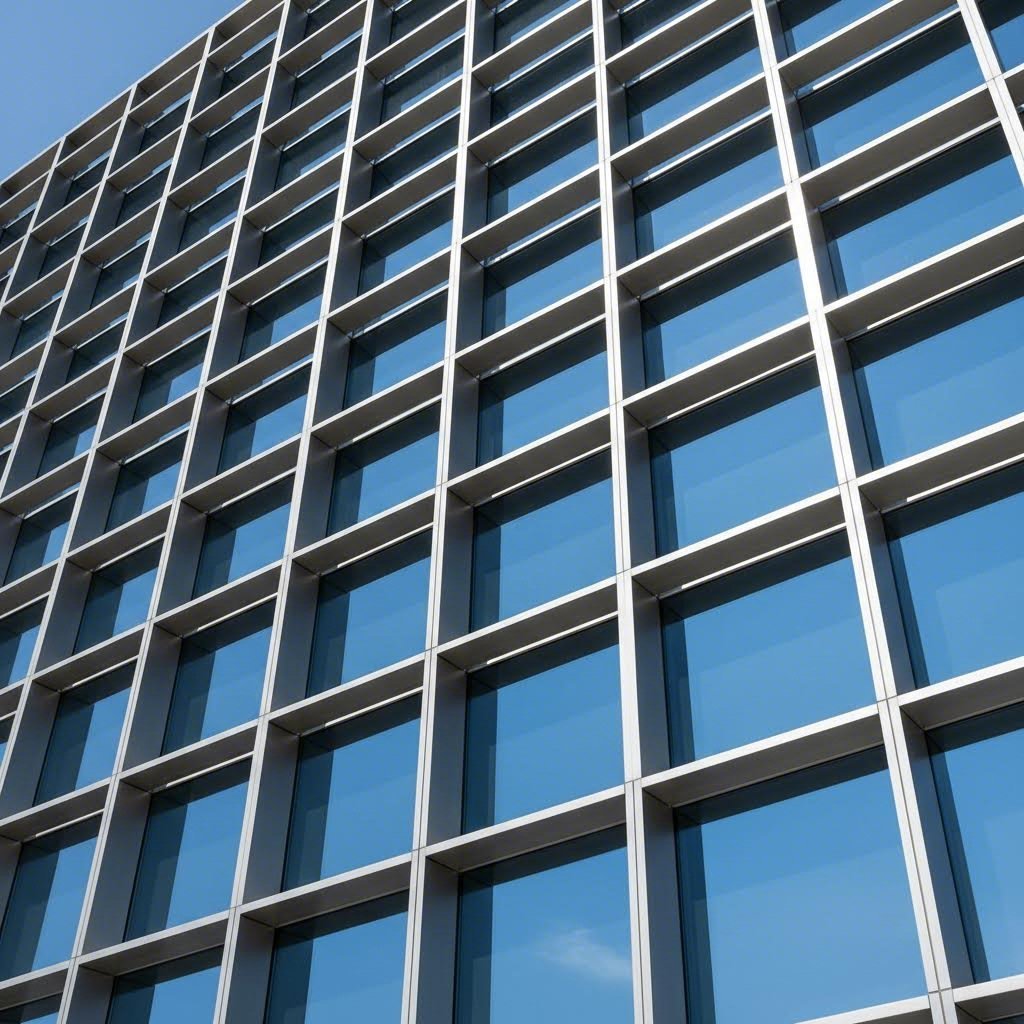
You understand the profile shapes, alloy grades, and surface finishes. But here's the practical question: which aluminum extrusions work best for your specific industry? The answer varies dramatically depending on whether you're designing a building facade, assembling a manufacturing cell, or engineering lightweight transportation components.
Let's bridge the gap between material knowledge and real-world application. Understanding how different industries prioritize profile characteristics helps you make selections that balance performance, aesthetics, and budget for your particular use case.
When you walk into any modern building, you're surrounded by extruded aluminium profiles. They frame the windows, support the curtain walls, and provide structural frameworks for storefronts and entrances. Why does architecture rely so heavily on aluminum extrusions? The combination of design flexibility, corrosion resistance, and elegant surface finishes makes them irreplaceable.
Here are the primary architectural applications where aluminum profiles excel:
What drives profile selection in architecture? Aesthetics typically lead the conversation. Surface finish quality, consistent color across large installations, and profiles with minimal visible fasteners take priority. Load-bearing requirements exist but rarely push beyond what 6063-T5 delivers. Most architectural profiles feature Class I anodizing or high-performance PVDF coatings for decades of weather exposure.
Step onto a manufacturing floor, and the priorities shift completely. Here, aluminum extrusions form the backbone of production infrastructure. Sounds different from architectural applications? It absolutely is. Industrial users care far less about surface finish and far more about load capacity, modularity, and assembly speed.
According to industry research, aluminum extrusions serve as the backbone of modern manufacturing operations across these critical categories:
The 8020 aluminum extrusion approach has transformed industrial facility design. Instead of welding steel frames that become permanent once assembled, manufacturers now build with reusable, reconfigurable components. When production lines change, the framing adapts rather than heading to the scrap bin.
Industrial profile selection criteria prioritize these factors:
Imagine designing a vehicle where every pound of weight reduces fuel efficiency or payload capacity. That's the reality for transportation engineers, and it explains why aluminum extrusions dominate modern vehicle construction.
Transportation applications include:
Transportation profile selection follows a distinct decision framework:
| Selection Factor | Architectural Priority | Industrial Priority | Transportation Priority |
|---|---|---|---|
| Surface Appearance | Critical | Low | Moderate |
| Load Capacity | Moderate | High | High |
| Weight Optimization | Low | Moderate | Critical |
| Corrosion Resistance | High | Moderate | High |
| Reconfigurability | Low | High | Low |
| Typical Alloy Choice | 6063-T5 | 6063-T5 / 6061-T6 | 6061-T6 / 7075-T6 |
Notice how the same profile type might serve completely different roles across industries. A square tube profile could frame a storefront entrance, support a conveyor structure, or reinforce a trailer floor. The application requirements, not the shape itself, determine the appropriate alloy grade, temper, wall thickness, and surface treatment.
Understanding these industry-specific priorities helps you communicate effectively with suppliers and ensures your profile specifications align with actual performance needs rather than assumptions. Whether you're sourcing standard catalog shapes or developing custom profiles, matching the selection criteria to your industry's priorities delivers better results at appropriate cost levels.
You've identified your industry application and understand which profile characteristics matter most. Now comes a pivotal decision that directly impacts your budget and timeline: should you select from an aluminum extrusion profile catalog or invest in custom die development? This choice affects everything from upfront costs to long-term production economics.
The answer isn't always obvious. Sometimes off-the-shelf solutions work perfectly. Other times, custom profiles deliver savings that dwarf their tooling investment. Let's break down exactly when each approach makes sense for your project.
Standard aluminum extrusions offer compelling advantages that shouldn't be overlooked. When you browse an extruded aluminum shapes catalog, you're seeing profiles refined through decades of market demand. These shapes exist because thousands of applications have proven their utility.
Consider standard aluminium profiles when your project aligns with these criteria:
The extensive variety available in any comprehensive aluminum profile catalog often surprises first-time buyers. Before assuming you need custom development, thoroughly review available standard options. You might find a standard aluminum extrusion that meets 90% of your requirements, with minor secondary machining handling the rest.
When does custom development become the smarter path? The answer typically involves volume, complexity, or both.
According to industry experts, the custom extrusion process begins with designing the desired profile shape using specialized software like AutoCAD or SolidWorks. These digital models enable faster quoting, streamlined prototyping, and reduced time to market. Once finalized, die development creates the precision tool that shapes every subsequent extrusion.
Custom profiles make economic sense when:
The die itself is a precision-machined steel disk, typically H13 grade, with openings cut to match your desired cross-section. Die complexity significantly affects both cost and lead time. Solid dies producing simple shapes cost less and manufacture faster than hollow dies requiring internal mandrels to create enclosed voids.
Understanding the true economics requires looking beyond die price tags. Here's how standard and custom options compare across critical factors:
| Factor | Standard Profiles | Custom Profiles |
|---|---|---|
| Initial Tooling Cost | $0 | $500 - $5,000+ depending on complexity |
| Per-Unit Cost (Low Volume) | Lower | Higher due to tooling amortization |
| Per-Unit Cost (High Volume) | Moderate | Often lower when secondary operations eliminated |
| Design Flexibility | Limited to catalog options | Virtually unlimited within extrusion constraints |
| Tooling Lead Time | None | 2-4 weeks typical |
| Production Lead Time | Days to weeks | Weeks after die approval |
| Minimum Order Quantity | Often 1 piece or 1 length | Typically 300-1,000+ pounds |
Why do minimum order quantities exist for custom work? Several practical reasons drive MOQ requirements:
Understanding what happens during tooling creation helps set realistic expectations. Tooling lead time typically runs 2-4 weeks, though intricate geometries may extend this timeline.
Die types affect both cost and capability:
After die completion, trial extrusions verify that the profile meets dimensional specifications. This testing phase consumes material but ensures production runs yield consistent, acceptable parts. Rushing this step invites quality problems that cost far more to resolve later.
Here's a strategy many buyers overlook: combining standard aluminum extrusion profiles with custom machining. This hybrid approach captures benefits from both worlds.
Imagine you need a profile with specific mounting holes, slots, or cutouts. Rather than developing a completely custom extrusion, you might select a close-fitting standard shape and add features through CNC machining. This works particularly well when:
The economics shift as quantities increase. At some crossover point, custom extrusion with integrated features costs less than machining standard shapes. That breakeven depends on profile complexity, machining extent, and order frequency. Working through the numbers with your supplier identifies the optimal approach for your specific situation.
Whether you source from an existing aluminum extrusion catalog or develop proprietary aluminium profiles, matching the approach to your actual requirements prevents both overspending on unnecessary tooling and underspending on solutions that create ongoing operational costs.
You've selected your profile type, alloy grade, and finish. But how do you know the extrusions you receive will actually fit your assemblies and perform as expected? The answer lies in understanding technical specifications and tolerances. These numbers might seem like fine print, but they directly determine whether your aluminum extrusion profiles slide together perfectly or require costly rework.
Industry standards establish the allowable variations from specified dimensions. Knowing what to expect, and what to demand, separates successful projects from frustrating ones.
Two primary standards govern aluminum extrusion sizes in North America: ASTM B221/B221M covers material specifications and mechanical properties, while ANSI H35.2 defines dimensional tolerances for aluminum mill products. Understanding both helps you communicate effectively with suppliers and set realistic expectations.
What exactly do these tolerances control? Every measurable characteristic of your extrusion profiles has defined limits:
Here's what many buyers don't realize: tolerances depend on profile size and complexity. According to industry tolerance charts, a dimension up through 0.124 inches on a profile with a circumscribing circle under 10 inches carries a standard tolerance of plus or minus 0.006 inches. That same dimension on a larger profile with a circumscribing circle of 10 inches or greater jumps to plus or minus 0.014 inches.
The distinction between "metal dimensions" and "space dimensions" matters significantly. Metal dimensions, where 75 percent or more of the measured distance is solid aluminum, hold tighter tolerances than space dimensions across open areas or voids. This affects how you design mating parts and specify critical features.
Weight calculations help verify that you're receiving the profile you ordered. Since aluminum extrusion sizes directly determine weight per foot, discrepancies signal potential problems with wall thickness or dimensional accuracy.
Calculating theoretical weight involves straightforward math. Multiply the cross-sectional area in square inches by the alloy density (approximately 0.098 lb/cubic inch for 6061) and the length in inches, then divide by 12 to get pounds per foot. Most suppliers publish weights for standard shapes, but custom profiles require calculation from the actual cross-section geometry.
When verifying extruded aluminum sizes against specifications, consider these factors:
Structural capacity depends directly on dimensional accuracy. A wall thickness at the low end of tolerance reduces section modulus and moment of inertia, meaning less load-carrying capability. For structural aluminium sections in load-bearing applications, specifying tighter precision tolerances may cost more but ensures predictable performance.
Beyond dimensions, surface quality classifications distinguish extrusion profiles suitable for different end uses. ASTM standards define allowable surface conditions including die lines, handling marks, and other imperfections.
The depth of surface conditions varies by wall thickness. Per industry specifications, profiles with wall thickness up through 0.063 inches allow surface conditions up to 0.0015 inches deep, while sections 0.501 inches and over permit conditions up to 0.008 inches deep. These limits apply to as-extruded surfaces before any finishing operations.
When evaluating supplier quality, request and verify these key specifications:
Just as you might reference a screw dimensions chart to verify fastener specifications, comparing extrusion documentation against industry standards confirms you're receiving conforming material. Similarly, understanding tolerances for aluminium sections parallels how builders use metal stud dimensions charts to ensure framing components meet specifications.
How tolerances affect your assemblies depends entirely on application requirements. Architectural trim fitting against building surfaces can absorb more variation than precision machine components requiring interference fits. Communicating your actual needs helps suppliers understand which dimensions are critical versus those where standard tolerances suffice. This dialogue often reveals opportunities to optimize specifications, reducing costs without sacrificing functionality.
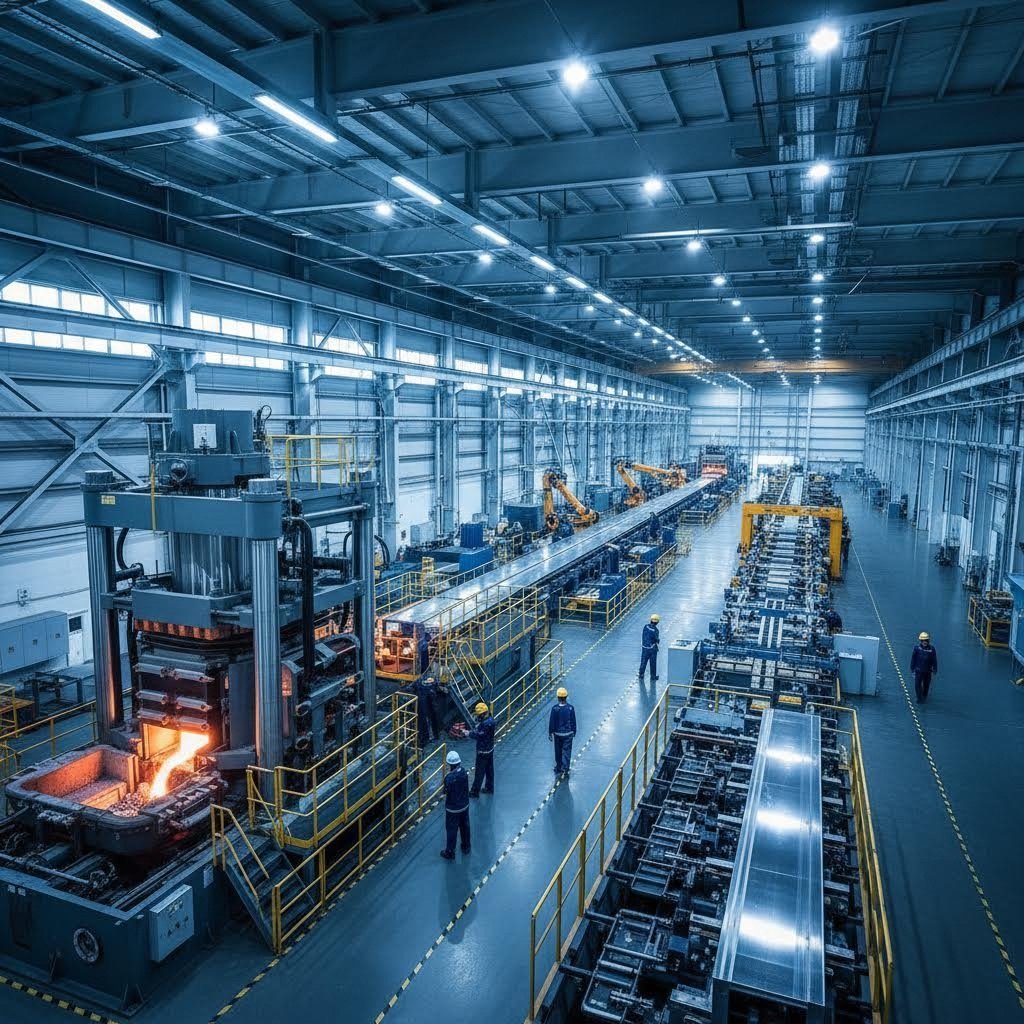
You understand specifications, tolerances, and quality standards. But where do you actually find aluminum extrusion profiles that meet your requirements? Sourcing decisions extend far beyond comparing prices on an aluminum extrusion catalog. The supplier you choose becomes a long-term partner whose capabilities directly impact your project success, timeline reliability, and total cost of ownership.
Whether you're looking for aluminium extrusions for sale in standard shapes or developing custom profiles for specialized applications, evaluating manufacturer capabilities systematically prevents costly mistakes and establishes relationships that serve you for years to come.
Not all extrusion suppliers offer the same capabilities. Some operate as distributors reselling stock aluminum extrusions from various mills. Others maintain full manufacturing operations with integrated processing. Understanding what a supplier can actually do, rather than what they claim, determines whether they can truly support your requirements.
When assessing where to buy aluminum extrusion, evaluate these critical capability areas:
Manufacturers like Shengxin Aluminium, with over 30 years of experience and comprehensive in-house capabilities, exemplify the integrated approach that reduces coordination complexity. Their combination of extensive press capacity, CNC machining centers, and multiple surface treatment options including anodizing, powder coating, PVDF, and micro-arc oxidation provides end-to-end support from die development through mass production.
Before committing to any supplier, ask targeted questions that reveal their true capabilities and reliability. Surface-level conversations don't expose the operational details that matter most for your projects.
According to industry guidance, partnering with the right aluminum firm is crucial to product success. Here are the essential questions to ask prospective suppliers:
Pay attention to how suppliers respond. According to procurement best practices, capable extrusion factories provide feasibility and cost optimization suggestions proactively, share inspection photos and reports before shipment, and prevent issues rather than reacting after defects occur.
The best sourcing relationships evolve beyond transactional purchasing. When you find a supplier whose capabilities align with your needs, developing that relationship creates ongoing value for both parties.
What does a true production partnership look like? Consider these relationship characteristics:
Factory-direct relationships with established manufacturers offer particular advantages for custom 6063 aluminum tubes, architectural profiles, and industrial applications. When browsing an aluminum profile catalog from a manufacturer rather than a distributor, you're seeing their actual production capabilities rather than aggregated offerings from multiple sources.
For projects requiring aluminum extrusion profiles catalog quantities or custom development, manufacturers with integrated capabilities streamline the entire process. Die development, extrusion, surface treatment, and secondary machining happen under one roof with unified quality control. This integration eliminates the coordination burden of managing multiple vendors and reduces opportunities for miscommunication or quality inconsistencies between process steps.
The investment in evaluating suppliers thoroughly pays dividends across every subsequent order. Once you've identified partners whose capabilities, communication style, and quality systems align with your requirements, the sourcing process becomes predictable rather than stressful. That foundation of supplier confidence lets you focus on designing great products rather than worrying about whether your aluminum will arrive correctly.
You've evaluated suppliers and understand their capabilities. But here's the question that ultimately drives every purchasing decision: what will your aluminum extrusion profiles actually cost? The answer involves far more than a simple per-foot price. Understanding the complete cost structure helps you budget accurately, compare quotes meaningfully, and identify optimization opportunities that competitors miss.
Whether you're sourcing standard alu profile shapes or developing custom aluminum profile extrusion solutions, the same fundamental cost drivers apply. Let's break down exactly what you're paying for and how to get the best value.
Every quote you receive reflects a combination of factors that suppliers weigh differently. Understanding these components transforms confusing price variations into logical differences you can evaluate.
According to industry research, aluminum prices rose sharply from around $1,500 per ton in 2020 to over $2,500 per ton in 2021, then stabilized around $2,200 per ton. These commodity fluctuations directly impact your extrusion aluminum costs since raw material typically represents 40-60% of the final price.
Here are the primary cost components that determine your aluminium extrusion profile pricing:
Profile design directly affects extrusion efficiency. Wall thickness, cross-sectional complexity, and tolerance requirements all influence how fast material moves through the press and how much ends up as scrap. According to design guidelines, increasing fillet radius from 0.8 mm to 1.5 mm in heavy-duty extrusions can significantly reduce die wear and improve surface finish, lowering long-term costs.
Sounds straightforward so far? Here's where many buyers get surprised. The quoted price rarely represents your total expenditure. These often-overlooked costs can significantly impact your budget:
Custom aluminum profiles can cost 30% to 50% more than standard profiles due to additional design and tooling requirements. However, this premium often disappears or reverses at higher volumes when you factor in eliminated secondary operations and reduced assembly complexity.
Now for the good news: multiple strategies exist to optimize your types of aluminum extrusions spending without sacrificing quality or performance.
Volume leverage: The relationship between order quantity and per-unit pricing is dramatic. Industry experience shows that shifting from a 1,000 kg order to a 10,000 kg order can reduce cost per meter by around 30%. Fixed costs like tooling and setup spread across more units while production efficiency improves.
Design optimization: Simplifying geometry reduces tooling cost, improves production speed, and minimizes waste. Work with your supplier's engineering team during design development to identify cost-reduction opportunities before finalizing specifications.
Alloy and temper selection: Don't overspecify. Using 6063-T5 where adequate saves money compared to 6061-T6, which costs more due to additional heat treatment and higher alloy content.
Factory-direct sourcing: Working directly with manufacturers rather than distributors eliminates middleman markups. Integrated manufacturers like Shengxin Aluminium offer competitive pricing through comprehensive in-house capabilities, combining extrusion, surface treatment, and CNC machining under one roof. This integration eliminates coordination costs and markup stacking that occurs when multiple vendors handle different process steps.
Total cost of ownership analysis: The cheapest extrusion isn't always the most economical choice. Consider:
When evaluating multiple suppliers, surface-level price comparison leads to poor decisions. One industry comparison revealed that Supplier A quoting US$2.50/m on 2,000 m actually cost less than Supplier B quoting US$2.30/m, because Supplier B's quote assumed 10,000 m volume and excluded finishing. Adjusted for equivalent terms, Supplier B's real cost came to US$2.80/m.
Request detailed breakdowns showing:
Verify that alloy grade, temper, tolerances, and finish specifications match across all quotes. A lower price for a different specification isn't a valid comparison.
The effort invested in understanding cost structures pays ongoing dividends. When you know what drives pricing for aluminum profile extrusion, you can make design decisions that optimize value, negotiate from an informed position, and identify suppliers whose pricing reflects genuine efficiency rather than hidden compromises in quality or service.
6063 aluminum is the architectural standard, offering superior surface finish and excellent anodizing response, making it ideal for window frames and decorative applications. 6061 aluminum delivers approximately 25-30% higher tensile strength in T6 temper, making it the preferred choice for structural applications, machine frames, and load-bearing components. The chemical composition differs too: 6061 contains higher concentrations of magnesium and silicon, which boost strength after heat treatment.
Custom aluminum extrusion dies typically range from $500 to $5,000 or more, depending on complexity. Solid dies for simple shapes cost less, while hollow dies requiring internal mandrels for tubes and enclosed voids are more expensive. Die costs are usually amortized across your order quantity. For example, a $1,500 tooling cost spread across a 2,000 kg order adds approximately $0.75 per kg. Custom profiles become economically viable at higher volumes when eliminated secondary operations offset the tooling investment.
T-slot aluminum profiles are modular framing solutions featuring continuous grooves that accept specialized hardware for tool-free assembly. They're widely used for machine frames, safety guarding, workstations, conveyor systems, and automation equipment. Brands like 80/20 popularized this system. The key advantage is reconfigurability: components can be repositioned, added, or modified without welding or drilling, making them ideal for manufacturing environments where production layouts evolve.
Major finishing options include anodizing (clear, colored, or hardcoat), powder coating, and PVDF coatings. Anodizing creates a protective oxide layer that becomes part of the metal, offering excellent durability and color options including black, bronze, and champagne. Powder coating provides virtually unlimited colors with good UV resistance. PVDF coatings meet the highest architectural standards for 30+ year exterior durability. Mill finish (unfinished) works for interior applications or when profiles undergo further processing.
Custom aluminum extrusions typically require minimum orders of 300-1,000 pounds or more, depending on the manufacturer and profile specifications. MOQs exist because die preparation, press setup, and quality verification take time regardless of order size. Larger profiles using bigger presses generally have higher MOQ thresholds. For lower volume needs, consider standard catalog profiles with custom machining as an alternative, or work with manufacturers like Shengxin Aluminium that offer flexible production capabilities across 35 extrusion presses.


 online service
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 English
 français
 Deutsch
 русский
 español
 português
 العربية
 ไทย
 Việt
 Українська