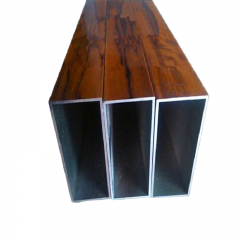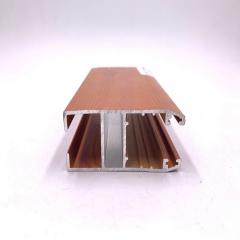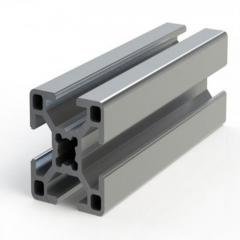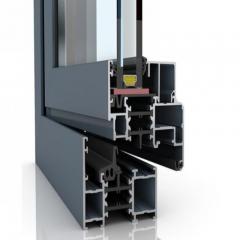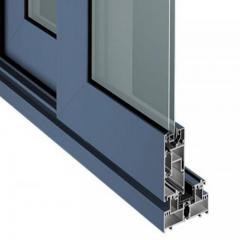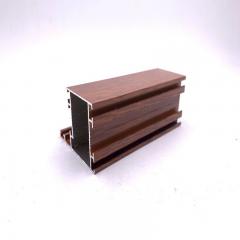
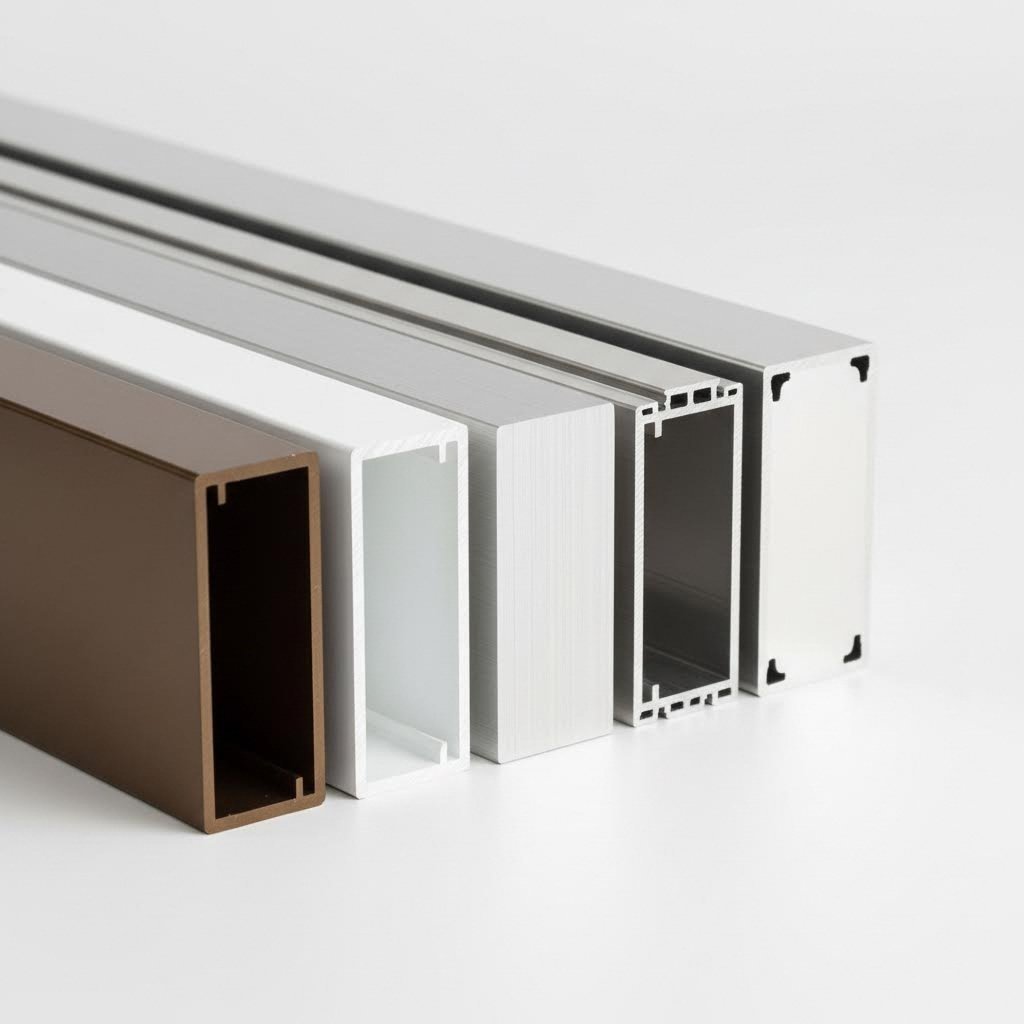
When you picture aluminum extrusion profiles coming off the production line, you might assume they're ready for immediate use. After all, aluminum is naturally corrosion-resistant, right? While that's partially true, raw extruded aluminum profiles rarely go directly into their final applications. Instead, they undergo finishing services for aluminum extrusions—a collection of surface treatments that transform basic aluminum shapes into components ready for demanding real-world environments.
These finishing processes aren't optional upgrades. They're essential steps that determine how well your aluminum profiles will perform over years of service. Whether you're working with standard aluminum shapes or curved aluminum extrusion designs, the right finish makes the difference between components that thrive and those that fail prematurely.
Here's something that might surprise you: aluminum does form a natural protective oxide layer when exposed to air. This thin film offers some baseline corrosion resistance, which is why aluminum doesn't rust like steel. However, this natural barrier is extremely thin—only about 2 to 3 nanometers—and provides minimal protection against mechanical wear, chemical exposure, or harsh environmental conditions.
Think about where extruded aluminum profiles actually end up. Architectural facades face decades of UV exposure and weather cycling. Marine components encounter salt spray daily. Industrial equipment endures constant abrasion and chemical contact. In each case, that microscopic natural oxide layer simply isn't enough.
Proper finishing treatments can extend aluminum component lifespan by 3 to 10 times compared to untreated surfaces, depending on the application environment and selected finish type.
Beyond protection, there's another practical consideration. Raw aluminum has a somewhat dull, industrial appearance that doesn't meet aesthetic requirements for consumer products, architectural elements, or visible components. Surface treatments solve both problems simultaneously.
Finishing services for aluminum extrusions serve two interconnected purposes that manufacturers must balance based on their specific application needs:
Functional Protection: This includes enhanced corrosion resistance through thickened oxide layers or protective coatings, improved wear resistance for components facing mechanical stress, and thermal or electrical properties modification. According to industry expertise from Rapid Axis, treatments like anodizing create durable barriers against moisture, chemicals, and salt spray—critical for aerospace, electronics, and architectural applications.
Aesthetic Enhancement: Surface treatments enable color customization ranging from subtle metallic tones to vibrant hues, various texture options from mirror-polished to matte finishes, and consistent appearance across production runs. This flexibility allows unique extrusions to match specific design requirements while maintaining their protective qualities.
The beauty of modern finishing methods is that you rarely have to choose between protection and appearance. Anodizing, for instance, simultaneously builds a harder protective surface while enabling decorative coloring. Powder coating delivers excellent scratch resistance alongside virtually unlimited color options. Understanding these dual benefits helps you select the right treatment for your aluminum profiles—whether they're standard catalog items or custom-designed components for specialized applications.
Here's a critical truth that many people overlook: the success of any finishing service for aluminum extrusions depends almost entirely on what happens before the actual coating or treatment begins. You can select the most advanced anodizing process or premium powder coating system available, but if the aluminum extrusion profile wasn't properly prepared, you're setting yourself up for failure.
Think of it this way—would you paint a wall without cleaning off the dirt and dust first? The same principle applies to aluminum, only the stakes are much higher. Surface preparation removes contaminants, activates the metal surface, and creates ideal conditions for finishes to bond properly. Skip these steps or rush through them, and you'll face adhesion failures, uneven appearances, and coatings that peel away far sooner than they should.
The moment aluminum extruded profiles come off the extrusion press, they're already picking up contaminants. Oils from the aluminium extrusion die, handling lubricants, airborne particles, and fingerprints from workers all accumulate on the surface. According to Gabrian International, oxygen exposure also causes initial oxidation, creating a greyish smut layer that must be removed before any finish can be applied.
The cleaning process typically involves multiple stages designed to address different types of contamination:
What makes this particularly important for profile aluminum applications? Even microscopic contamination creates weak points where coatings won't bond correctly. These invisible flaws become visible problems later—blistering, peeling, or accelerated corrosion that compromises the entire component.
After cleaning comes etching—a controlled chemical process that removes a thin layer of aluminum to create a uniform, activated surface. This step accomplishes several things simultaneously. It eliminates surface irregularities, removes embedded contaminants that cleaning couldn't address, and creates microscopic texture that dramatically improves coating adhesion.
As explained by Dorsetware, proper etching evens out surface defects and micro-scratches, leading to more consistent oxide layers during anodizing. For color anodizing specifically, etched surfaces allow deeper and more uniform dye absorption, resulting in richer, more consistent tones.
The complete preparation sequence for aluminum extrude surfaces typically follows this order:
Research from Boeing's chemical technology division reveals just how precise this process must be. Their studies found that the combination of short deoxidizer immersion times and incorrect rinse durations can leave invisible smut residue on surfaces. Parts appear clean and even pass water-break-free tests, yet this hidden contamination leads to catastrophic paint adhesion failures during assembly.
The consequences of inadequate preparation extend beyond immediate failures. Aluminium extrusion dies produce profiles with consistent geometry, but surface quality varies based on extrusion conditions. Without proper preparation, these variations become magnified in the final finish—some sections bond perfectly while others show inconsistencies that only become apparent months or years later.
This is precisely why experienced finishing service providers invest heavily in their preparation processes and monitor chemical concentrations continuously. The finishing method you ultimately choose matters significantly, but it can only perform as well as the surface preparation allows.
Now that you understand why proper surface preparation matters, let's explore the most widely used finishing method for custom aluminum extrusions: anodizing. This electrochemical process doesn't simply coat the aluminum surface—it actually transforms it, creating a protective layer that becomes part of the metal itself. That fundamental difference is what makes anodizing so effective for applications ranging from architectural facades to aerospace components.
According to Valence Surface Technologies, aluminum ranks as the second most widely used metal in the world, and anodizing has become the go-to method for enhancing its properties. Whether you're working with standard aluminum extrusion shapes or a bespoke aluminium extrusion designed for specific requirements, understanding how anodizing works helps you make informed decisions about your finishing specifications.
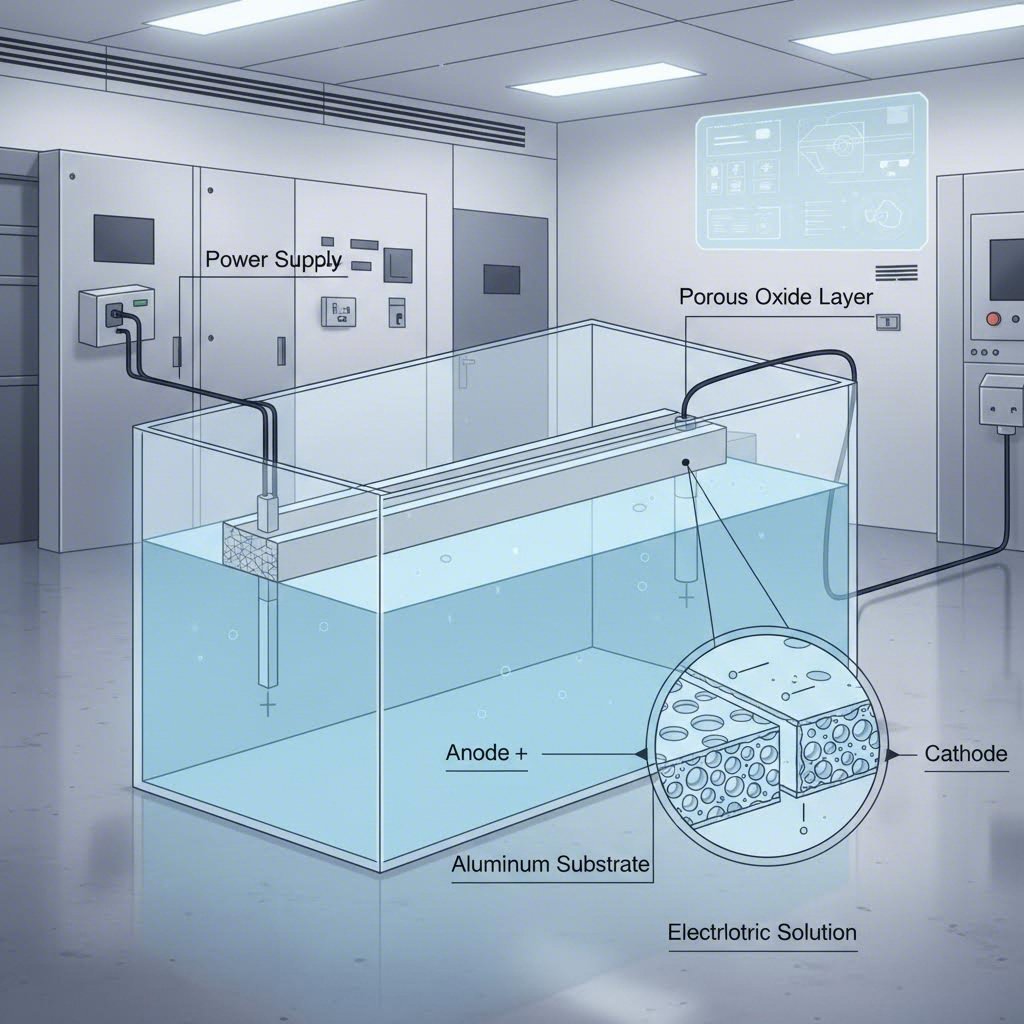
Imagine submerging your aluminum component in an acid bath while running electrical current through it. Sounds destructive, right? Actually, this controlled electrochemical reaction produces remarkable results. The aluminum serves as the positive electrode (anode) in an electrolytic cell, which is where the name "anodizing" comes from.
Here's what happens at the molecular level: when electrical current passes through the acidic solution, oxygen ions are released and combine with aluminum atoms on the surface. This forms aluminum oxide (Al2O3)—an extremely hard, corrosion-resistant compound that grows outward from the metal surface while simultaneously penetrating into it.
The process follows several key stages:
What makes anodized surfaces so resistant to corrosion? The aluminum oxide layer is chemically stable and bonds directly with the base metal rather than sitting on top like paint or plating. This integral bond means it won't chip, peel, or flake away under normal conditions. Even if the surface gets scratched, the underlying aluminum simply re-oxidizes naturally, providing ongoing protection.
Not all anodizing processes are created equal. The military specification MIL-A-8625F defines three primary types, each offering distinct characteristics suited to different applications. Understanding these differences helps you specify the right treatment for your custom aluminum products.
Type I produces the thinnest oxide layer and is often specified when you need improved paint adhesion without significant dimensional changes. It's particularly valuable for small aluminum extrusions in aerospace applications where every thousandth of an inch matters.
According to Accurate Metal, Type II is the most commonly specified anodizing process. The minimal buildup—typically around 0.0007 inches with half penetrating into the alloy—means parts rarely require masking for dimensional concerns. This makes it cost-effective for high-volume production of architectural and decorative components.
Type III hardcoat creates a surface so hard it rivals tool steel. As noted by industry experts at Accurate Metal, this coating forms an excellent base for dry film lubricants, Teflon, paint, and adhesives. However, the thicker buildup requires careful consideration during design—approximately half the coating builds up from the surface while half penetrates into the base metal.
One critical limitation to remember: you cannot layer anodizing treatments. You can't hardcoat over existing hardcoat, add anodize over anodize, or simply build up additional thickness later. This means specifying the correct type upfront is essential for your application requirements.
| Characteristic | Type I (Chromic) | Type II (Sulfuric) | Type III (Hardcoat) |
|---|---|---|---|
| Thickness Range | Up to 0.0001" | 0.0002" - 0.001" | 0.001" - 0.004" |
| Hardness | Low | Moderate | Very High |
| Color Options | Limited (gray) | Extensive | Gray to black, dyeable |
| Wear Resistance | Minimal | Good | Excellent |
| Cost | Moderate | Lowest | Highest |
| Dimensional Impact | Negligible | Minimal | Significant |
The versatility of anodizing explains its dominance among finishing services for aluminum extrusions. From the subtle, durable finishes on architectural window frames to the battle-hardened surfaces of military equipment, this electrochemical process adapts to meet diverse performance requirements. When paired with proper alloy selection—which we'll explore in detail later—anodizing delivers consistent, long-lasting results that few other finishing methods can match.
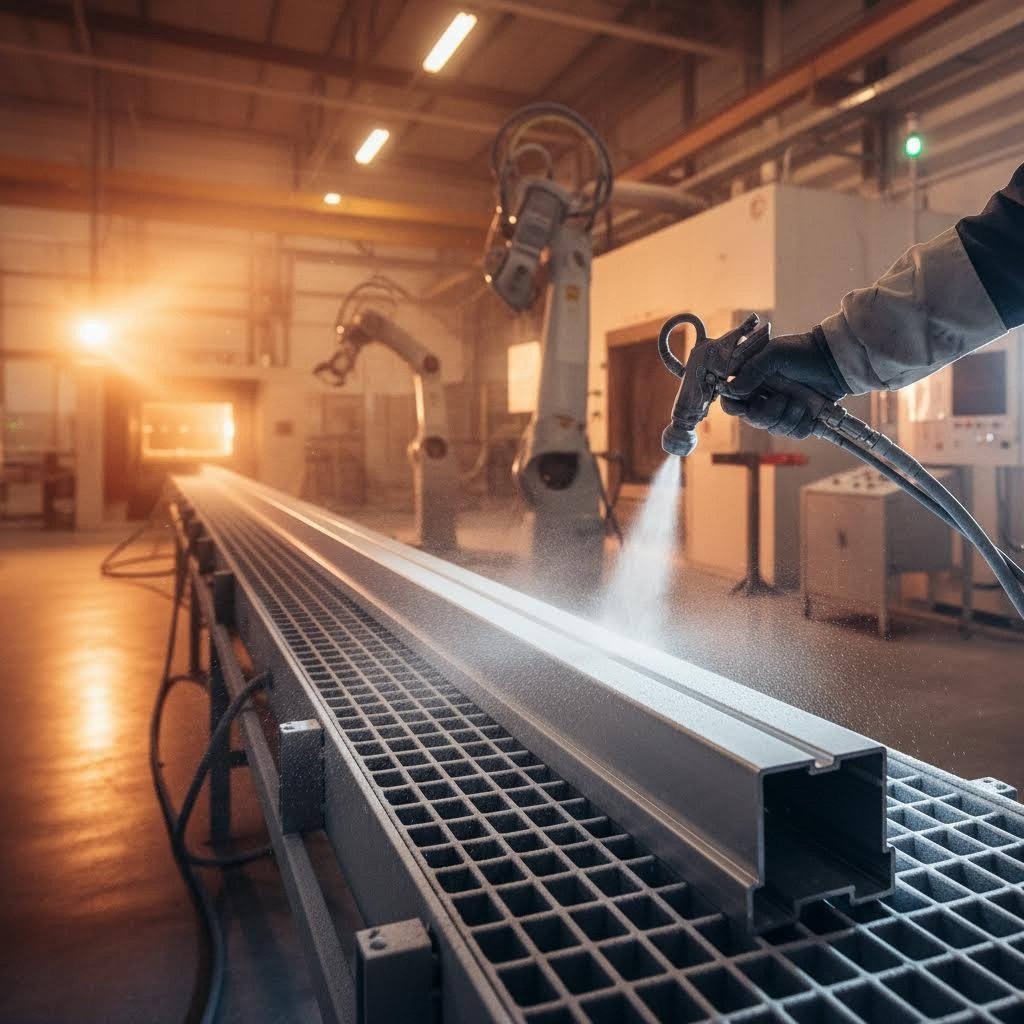
While anodizing transforms the aluminum surface itself, powder coating and liquid paint systems take a different approach—they create a protective barrier on top of the metal. For many custom aluminum applications, these coating methods offer advantages that anodizing simply can't match, particularly when it comes to color selection and texture versatility. Understanding how each process works helps you determine which finishing method best suits your extrusion profiles.
Both options have earned their place in the industry, and as Master Craft Finishers notes, the choice between paint and powder coatings for aluminum profile applications remains one of the most discussed topics among architects, fabricators, and processors. Let's break down what makes each method unique.
Imagine spraying dry, finely ground particles onto metal and having them stick perfectly without any liquid involved. That's essentially what happens during powder coating. The process uses electrostatic attraction to bond dry powder particles to the aluminum surface before heat transforms them into a smooth, durable finish.
Here's how the electrostatic application works: the powder particles receive a positive electrical charge as they pass through a specialized spray gun. Meanwhile, the aluminum extrusion trim or component is grounded, creating a negative charge. Opposite charges attract, so the charged powder particles cling uniformly to all surfaces of the part—even reaching into recesses and around corners that would challenge traditional spray painting.
After coating, the parts move into curing ovens where temperatures typically reach 350-400°F. This heat triggers a chemical reaction that melts and fuses the powder particles into a continuous film. Unlike paint that dries through solvent evaporation, powder coating actually crosslinks at the molecular level, creating an exceptionally tough surface.
What makes powder coating attractive for custom extrusions? According to industry experts, the advantages are substantial:
Texture options for powder coating include:
Gloss levels span the full spectrum:
However, powder coating isn't without challenges. Color matching often requires larger minimum order quantities compared to liquid paints. Surface imperfections like orange peel texture can occur if application parameters aren't precisely controlled. And here's something that catches many people off guard—extruded aluminum trim that's been powder coated is significantly harder to touch up or repair than painted surfaces. If a part gets damaged, blending repairs seamlessly becomes difficult.
For architectural applications where long-term color stability is paramount, PVDF (polyvinylidene fluoride) coatings—commonly known by the trade name Kynar—have been the gold standard since 1965. These liquid paint systems deliver performance characteristics that powder coatings are only now beginning to match.
PVDF coatings require a more complex application process than powder. According to Linetec's technical specifications, proper application includes pretreatment, primer application, and topcoat—all by curing at approximately 450°F. This multi-layer approach creates exceptional adhesion and durability.
What sets PVDF apart for aluminium extrusion trim and architectural aluminum profiles?
Texture and gloss options for PVDF systems include:
The trade-offs? PVDF paints cost more than powder coatings. The higher curing temperatures can be problematic for components with thermal breaks or thin sections. And environmental concerns around VOC content have pushed some specifiers toward powder alternatives.
Recent advances have narrowed the performance gap significantly. As noted by Master Craft Finishers, powder coating formulations now achieve AAMA 2605 certification—the same high-performance standard that PVDF finishes meet—with warranties extending to 20-30 years.
For aluminum profile applications, consider these durability factors when choosing between methods:
| Performance Factor | Powder Coating | PVDF Paint |
|---|---|---|
| Impact Resistance | Excellent | Good |
| UV/Color Stability | Very Good (AAMA 2605) | Excellent (proven history) |
| Repairability | Difficult | Easier |
| Environmental Impact | Low/No VOCs | Higher VOCs |
| Gloss Range | Full spectrum | Limited to 40 max |
| Minimum Order Size | Larger for custom colors | Smaller custom batches |
| Application Restrictions | Broader facility options | Licensed applicators only |
The bottom line? Both powder coating and PVDF have distinct advantages that make them valuable for different situations. Powder coatings excel in impact resistance, environmental sustainability, and aesthetic variety. PVDF delivers unmatched consistency, proven longevity, and flexibility for specialized color requirements. For custom extrusions destined for architectural applications, your choice often comes down to specific project demands, environmental considerations, and long-term maintenance expectations.
Of course, coating methods represent just one category of surface treatment. When your application calls for specific textures or visual effects that neither anodizing nor coating can achieve, mechanical finishing techniques offer another powerful set of options.
Sometimes the best finish isn't a coating at all—it's what you can achieve by physically altering the aluminum surface itself. Mechanical finishing uses abrasives, brushes, and specialized tools to create textures and appearances that chemical treatments simply can't replicate. Whether you need a mirror-like reflection for decorative applications or a subtle brushed grain that hides everyday wear, these techniques give you precise control over your extruded aluminum shapes' final appearance.
What makes mechanical finishing particularly versatile? It can serve as either a standalone treatment or as preparation for subsequent chemical processes. According to Empire Abrasives, mechanical finishes have played a major role in metalworking for centuries, affecting both aesthetics and functionality across industries from automotive to architecture. For extrusion shapes used in consumer products or architectural elements, the right mechanical finish often determines whether a component looks premium or ordinary.
Want your aluminum to reflect like glass? That's exactly what polishing achieves. This process progressively removes surface imperfections using increasingly finer abrasives until the metal reaches your desired reflectivity level. The key word here is "progressively"—you can't jump straight to fine polishing compounds and expect good results.
The grit progression typically works like this:
As Prolean Tech explains, polished aluminum reflects light extremely well and requires this multi-stage buffing process to achieve that mirror-like surface. Skipping grit stages leaves scratches from previous steps visible in the final finish—a mistake that's immediately obvious under good lighting.
Common mechanical finish designations and their characteristics include:
Where do polished extruded shapes make the most sense? Lighting fixtures, decorative trim, signage, and applications where reflectivity adds functional or aesthetic value. However, there's a practical consideration: polished aluminum shows fingerprints, scratches, and wear more readily than textured finishes. For high-traffic applications, a brushed or matte finish often proves more practical.
Brushed finishes create that distinctive linear grain pattern you've seen on appliances, electronics, and architectural elements. Unlike polishing, which aims to eliminate all visible texture, brushing intentionally creates fine parallel lines across the aluminum surface. The result? A sophisticated appearance that actually hides minor scratches and everyday wear.
The brushing process involves moving an abrasive material—typically wire brushes, abrasive pads, or sanding belts—across the aluminum in a single, consistent direction. This creates the characteristic grain pattern where the coarseness of your abrasive determines the depth and width of the lines. According to Wayken RM, brushing removes surface imperfections while creating unidirectional lines parallel to the brushing direction, giving aluminum products an air of luxury.
Directional considerations matter significantly for brushed finishes:
Beyond brushing, other textured finishes expand your options for alum extrusion shapes:
Here's something worth noting: mechanical finishing can serve as either the final treatment or as preparation for chemical finishing. When flextrude aluminum shapes or other custom profiles will undergo anodizing, a pre-treatment brushing or polishing step determines the final appearance. The anodizing process preserves the mechanical texture beneath its protective oxide layer, so the base finish directly influences the end result.
For standalone applications, brushed aluminum offers practical advantages. As industry experts note, brushed aluminum is more durable against scratches and better suited for everyday use than polished surfaces. Adding an anodized layer over a brushed finish creates even tougher, more corrosion-resistant surfaces suitable for outdoor applications, moisture environments, and industrial settings.
Choosing between mechanical finishes ultimately depends on your end-use requirements. High-visibility decorative applications might demand mirror polishing despite its maintenance challenges. Consumer electronics and appliances typically benefit from brushed finishes that balance appearance with practicality. Industrial components often use bead blasting or matte finishes where functionality trumps aesthetics. Understanding these trade-offs helps you specify the right mechanical treatment—and determine whether additional chemical finishing will enhance your results.
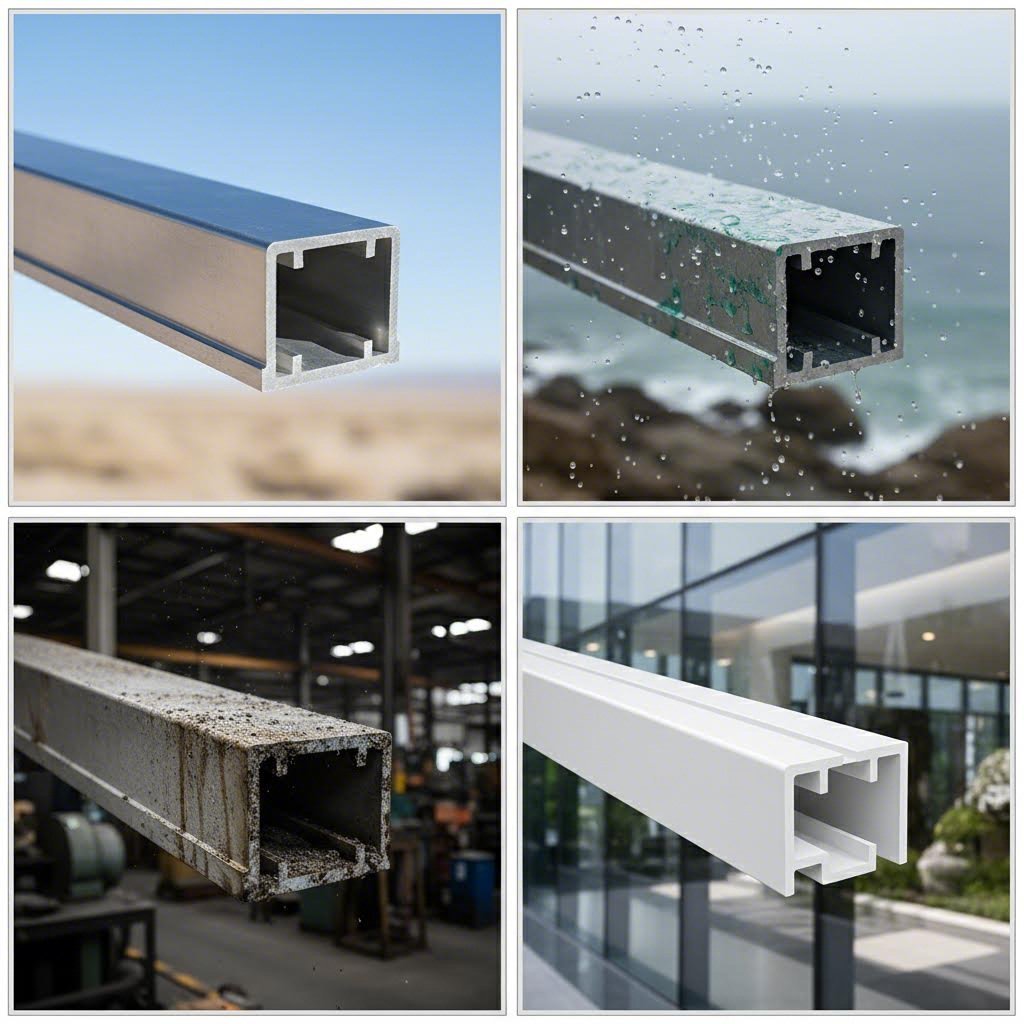
You've now explored anodizing, powder coating, PVDF, and mechanical finishing as individual processes. But here's the real question: which method actually works best for your specific application? The answer depends on where your aluminium extrusion will spend its working life and what environmental challenges it needs to withstand.
Selecting the right finish for aluminum profile extrusion isn't just about aesthetics—it's about matching performance characteristics to real-world conditions. A finish that excels on architectural facades might fail completely in marine environments. Understanding these distinctions helps you avoid costly mistakes and ensures your components perform reliably for years.
When aluminum extrusion companies discuss durability, they're really talking about several distinct performance factors. Each finishing method excels in different areas, and understanding these trade-offs guides better specification decisions for both stock aluminum extrusions and custom extruded profiles.
Let's break down how each method performs across key criteria:
| Criteria | Anodizing (Type II/III) | Powder Coating | PVDF Paint | Mechanical Finish |
|---|---|---|---|---|
| UV Resistance | Excellent—integral oxide layer doesn't fade | Very Good—AAMA 2605 rated options available | Excellent—50+ year proven track record | Poor—requires additional protective coating |
| Salt Spray Resistance | Excellent—particularly Type III hardcoat | Good to Very Good—depends on pretreatment quality | Very Good—multi-layer system provides protection | Poor—no inherent corrosion protection |
| Chemical Exposure Tolerance | Very Good—resists most mild chemicals | Good—varies by powder formulation | Excellent—fluoropolymer chemistry resists solvents | Poor—unprotected aluminum surface |
| Abrasion Resistance | Excellent (Type III)—hardness rivals tool steel | Good—impact resistant but can scratch | Moderate—softer than powder coating | Variable—depends on subsequent treatment |
| Relative Cost | Moderate to High | Low to Moderate | High | Low to Moderate |
| Color Options | Moderate—dye-based, limited to certain tones | Extensive—virtually unlimited colors and textures | Extensive—excellent color matching capability | None—natural aluminum appearance only |
| Coating Thickness | 0.0002" - 0.004" depending on type | 0.002" - 0.006" typical | 0.001" - 0.002" typical | N/A—surface modification only |
| Repairability | Difficult—cannot re-anodize selectively | Difficult—touch-ups visible | Good—field repairs possible | Good—can re-polish or re-brush |
What patterns emerge from this comparison? Anodizing delivers the best combination of hardness and corrosion resistance, making it ideal for aluminium extrusion profiles facing mechanical stress or harsh chemical environments. Powder coating offers the most versatility at competitive pricing—particularly valuable when color matching or texture variation matters. PVDF excels in long-term architectural applications where color stability and repairability justify higher costs. Mechanical finishes, while attractive, require additional protective treatments for any outdoor or demanding application.
According to Gabrian International, anodizing is ideal when you need tight dimensional margins, outstanding corrosion and wear resistance, and an attractive metallic look. Meanwhile, powder coating might be the solution if you're seeking vibrant colors or unique textures that will last even when exposed to the elements.
Environmental exposure varies dramatically across applications. The finish that protects aluminium extrusion profiles on a commercial building in Arizona faces completely different challenges than one used on a boat in Florida. Here's how to match finishes to specific conditions:
Building facades, window frames, curtain walls, and storefronts demand finishes that maintain appearance over decades of UV exposure and weather cycling. For extruded profiles in architectural use, consider:
As noted by Prance Building Materials, PVDF fluoropolymer coatings remain the industry standard for outdoor aluminum applications, offering excellent UV resistance, color retention, and chalk resistance backed by extensive warranties.
Salt spray creates one of the most aggressive corrosive environments for aluminum. Boats, docks, coastal structures, and offshore equipment require maximum corrosion protection:
Trim pieces, structural components, and decorative elements face road chemicals, stone chips, and thermal cycling. Custom extruded profiles for automotive use need:
Machinery, equipment housings, conveyor systems, and processing equipment encounter chemicals, abrasion, and heavy use:
Here's a practical decision framework based on your primary concerns:
According to Wrisco Industries, the finish you choose depends on your specific goals—prioritizing durability and color suggests anodized or painted aluminum, while sleek aesthetics point toward brushed or polished options. When budget and versatility matter most, mill finish aluminum with subsequent powder coating delivers reliable performance.
One factor that often gets overlooked in these comparisons? The aluminum alloy itself significantly influences which finishing methods work best. Different alloys respond differently to anodizing chemistry, accept coatings with varying adhesion levels, and polish to different degrees of reflectivity. Understanding this connection between base material and surface treatment helps you optimize both your extrusion specification and finishing selection.
Here's something that catches many engineers off guard: not all aluminum alloys respond the same way to finishing processes. You might specify a beautiful anodized finish only to discover that your chosen alloy produces inconsistent coloring or a mottled appearance. This disconnect between alloy selection and finishing outcomes represents one of the most overlooked aspects of custom aluminum extrusion design.
The reality? Your alloy choice during the extrusion design phase directly determines which finishing methods will deliver optimal results downstream. According to Global Metal Finishing, different alloys have unique properties that impact necessary finishing processes and the finished outcome. Understanding these connections before you fabricate aluminum components saves you from costly surprises during production.
What makes one alloy respond beautifully to anodizing while another produces disappointing results? It comes down to chemistry—specifically, the alloying elements that give each aluminum grade its distinct properties.
Silicon content plays a particularly critical role. High silicon levels interfere with the electrochemical process during anodizing, creating dark spots, uneven oxide layers, and colors that don't match your specifications. Copper content affects corrosion resistance after finishing. Magnesium influences how the oxide layer forms and accepts dyes. Each element contributes to the final outcome in ways that aren't always obvious until you've committed to a finishing process.
Here's how common extrusion alloys match up with different finishing methods:
As noted by American Douglas Metals, the 6063 alloy is the most popular for aluminum extrusions particularly because of its excellent extrudability, anodizing properties, and the high-quality surface finish it provides. When your extruded aluminium profiles require premium decorative finishes, this alloy delivers consistently superior results.
Why does 6063 dominate architectural and decorative applications? The answer lies in its carefully balanced composition. According to Metal Exchange, 6063 typically contains around 0.6% silicon and 0.9% magnesium—proportions that form magnesium silicide (Mg₂Si) during heat treatment. This compound provides moderate strength while keeping the surface chemistry ideal for anodizing.
The low silicon content is particularly important. During anodizing, silicon particles don't oxidize the same way aluminum does. They remain embedded in the growing oxide layer, scattering light and creating visual inconsistencies. With 6063's minimal silicon, these disruptions stay negligible, resulting in clear, uniform finishes that accept dyes evenly across the entire surface.
Consider what this means for profile precision extrusions destined for visible applications:
For custom extrusion aluminum projects where appearance matters, specifying 6063 from the start prevents finishing complications later. The alloy's excellent extrudability also means complex aluminum tube shapes and intricate profiles form cleanly, with smooth surfaces that require minimal preparation before finishing.
What if your application demands higher strength than 6063 provides? That's where thoughtful alloy-finish pairing becomes strategic. You might specify 6061 for structural components while using 6063 for visible trim pieces—both finished differently to optimize their respective strengths. Or you might accept 6061's anodizing characteristics for industrial applications where slight color variations don't impact functionality.
The key takeaway? Alloy selection and finish specification aren't separate decisions—they're interconnected choices that determine your final product quality. Working with manufacturers who understand these relationships helps you avoid mismatches that lead to rejected parts, production delays, or compromised appearance.
You've identified the right alloy for your project and determined which finishing method suits your application. Now comes a critical step that often separates successful projects from frustrating ones: choosing the right finishing service provider. Not all aluminum extrusion suppliers and finishers deliver the same quality, lead times, or expertise—and the differences become painfully obvious only after you've committed to a production run.
Think of your finishing partner as an extension of your manufacturing process. According to Light Metals Coloring, a quality finisher should work to become an extension of its customers' businesses, forging a lasting, mutually beneficial partnership. The right provider doesn't just apply coatings—they understand your application, anticipate potential issues, and communicate proactively throughout the process.
Before committing to any profile extrusion company or finishing specialist, you need clear answers to several critical questions. These conversations reveal whether a potential partner has the capabilities, experience, and commitment your project requires.
Start with these fundamental inquiries:
Beyond these basics, dig deeper into their process capabilities:
Consistent quality separates reliable custom extruded aluminum finishers from those who deliver unpredictable results. As industry experts note, inconsistent results could jeopardize the functionality of your products—and your business's reputation.
When evaluating potential providers, verify their quality credentials:
Third-party certifications matter because they demonstrate commitment beyond minimum requirements. According to finishing industry professionals, these certifications reinforce professionalism and responsibility while providing competitive advantages over uncertified providers.
Ask specifically about inspection processes throughout the workflow:
Before placing production orders, request samples whenever possible. For custom profile extrusion finishing, seeing actual results on representative parts prevents expensive surprises. Quality providers welcome sample requests because they understand how critical finish appearance is to your end product.
When requesting quotes from finishing service providers, provide these details upfront to receive accurate estimates and prevent miscommunication:
Understanding finish warranties protects your investment. Bristol aluminum and other quality providers typically offer warranties ranging from 1-5 years for standard industrial applications up to 20-30 years for architectural PVDF or AAMA 2605-rated powder coatings. However, warranties often include conditions about proper installation, maintenance, and environmental exposure. Review these terms carefully before assuming coverage applies to your specific use case.
The finishing workflow extends from your initial inquiry through final delivery. Reputable providers maintain clear communication at each stage—confirming specifications, reporting any issues discovered during preparation, and documenting inspection results. This transparency might seem like extra effort, but it prevents the costly rework and delays that plague relationships with less professional suppliers.
Of course, working with separate extrusion and finishing providers introduces coordination challenges. What if you could streamline this process by partnering with manufacturers who handle everything from die design through surface treatment?
What if you could eliminate the coordination headaches between separate extrusion and finishing providers entirely? That's precisely what integrated manufacturing offers. Rather than shipping your custom profile extrusions from one facility to another—managing multiple vendors, tracking separate timelines, and hoping everything aligns—integrated solutions consolidate the entire process under one roof.
This approach isn't just convenient. According to ALLWIN Hardware, controlling every stage of the extrusion process with strict quality standards and continuous improvement practices guarantees precision and reliability in every profile. When the same team handles die development, extrusion, machining, and surface treatment, quality control becomes seamless rather than fragmented across multiple suppliers.
Why are more manufacturers choosing single-source aluminum extrusion services over the traditional multi-vendor approach? The advantages compound at every stage of production—from initial design consultation through final delivery.
Consider what happens when you work with separate providers. Your extrusion arrives at the finishing facility, but did the finisher receive your exact specifications? Does their preparation process account for your specific alloy? If problems emerge during finishing, who's responsible—the extruder who produced the profile or the finisher who treated it? These coordination gaps create delays, disputes, and quality inconsistencies that integrated providers eliminate entirely.
Key advantages of single-source manufacturing and finishing include:
According to industry expertise from Star Extruded Shapes, experience and turn-key service offerings enable manufacturers to provide a complete manufacturing experience—setting them apart in the aluminum extrusion market. This end-to-end capability proves especially valuable for profile custom extrusions requiring precise tolerances and specific surface treatments.
What does comprehensive integrated service actually look like in practice? Leading custom aluminum extruders offer capabilities spanning the complete manufacturing workflow—from your initial design concept through finished, packaged components ready for assembly.
The journey typically begins with die development. Precision dies made from H13 steel are produced to create your desired cross-section. As industry sources note, high-quality die design ensures accuracy, material flow balance, and minimal production defects. When the same organization develops your dies and handles subsequent finishing, they can optimize designs for both extrudability and finishing outcomes.
After extrusion, many applications require secondary machining operations before surface treatment. This is where CNC capabilities become critical. Precise cutting, drilling, tapping, and bending must occur before finishing—you can't easily machine through anodized or powder-coated surfaces without damaging them. Integrated providers sequence these operations optimally, ensuring machined features receive proper edge treatment and don't compromise subsequent coating adhesion.
Shengxin Aluminium exemplifies this integrated approach, with over 30 years of industry experience delivering complete extrusion and processing services. Their facility houses 35 advanced extrusion presses ranging from 600T to 5500T capacity, alongside state-of-the-art CNC machining centers capable of precise cutting, drilling, and bending to meet exact specifications before finishing operations begin.
Surface treatment options from comprehensive providers typically span the full spectrum we've discussed throughout this guide:
This breadth of finishing capability matters because your application requirements might evolve. Perhaps you start with standard anodizing but later need hardcoat for a wear-critical component. Maybe your architect specifies PVDF for a new facade project. Working with providers offering multiple finishing methods gives you flexibility without switching vendors.
For manufacturers sourcing alumnium extrusion components at scale, the integrated model delivers measurable advantages. Reduced coordination complexity means fewer delays. Consolidated quality control means fewer rejected parts. And technical expertise spanning both extrusion and finishing means problems get identified and solved during design rather than discovered during production.
Whether you're developing prototypes or scaling to high-volume production, exploring integrated processing services helps you understand how consolidated manufacturing can streamline your supply chain while improving finished component quality. The investment in finding the right integrated partner pays dividends across every project—delivering consistent results that separate-vendor approaches struggle to match.
The primary finishing services include anodizing (Type I, II, and III), powder coating, PVDF liquid paint systems, and mechanical finishing techniques like polishing and brushing. Anodizing creates an integral oxide layer for corrosion resistance, powder coating offers unlimited color options with electrostatic application, PVDF provides proven 50+ year architectural performance, and mechanical finishing creates specific textures from mirror-polish to brushed grain patterns.
Choose anodizing when you need tight dimensional tolerances, superior wear resistance, or a metallic appearance—Type III hardcoat rivals tool steel hardness. Select powder coating when vibrant colors, unique textures, or cost-effectiveness matter most. For architectural applications requiring both durability and color stability, AAMA 2605-rated powder coatings now match PVDF performance with 20-30 year warranties.
The 6063 alloy contains approximately 0.6% silicon—low enough to prevent the dark spots and uneven oxide layers that higher silicon alloys produce. This composition creates exceptionally uniform, bright anodized surfaces that accept dyes evenly, making it ideal for architectural facades, decorative trim, and any application requiring consistent color matching across production runs.
Proper preparation includes solvent degreasing to remove oils, alkaline cleaning to break down contaminants, chemical etching to create uniform surface texture, deoxidizing to remove smut layers, thorough rinsing between each stage, and complete drying. Skipping these steps causes adhesion failures, uneven finishes, and premature coating degradation that may only appear months after installation.
Integrated providers like Shengxin Aluminium eliminate coordination headaches between separate vendors by handling die development, extrusion, CNC machining, and surface treatment under one roof. Benefits include streamlined communication, reduced lead times without inter-facility shipping, unified quality control, alloy-finish compatibility optimization, and single-point accountability for the entire manufacturing outcome.


 online service
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 English
 français
 Deutsch
 русский
 español
 português
 العربية
 ไทย
 Việt
 Українська