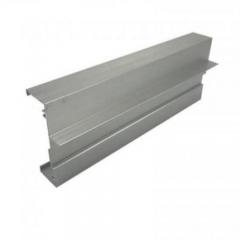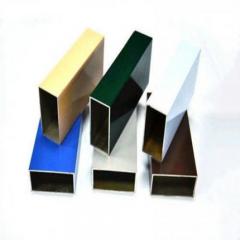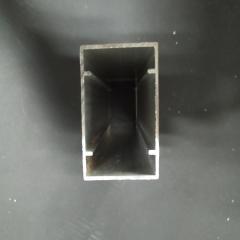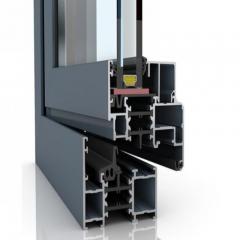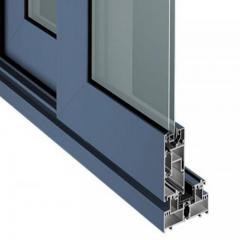
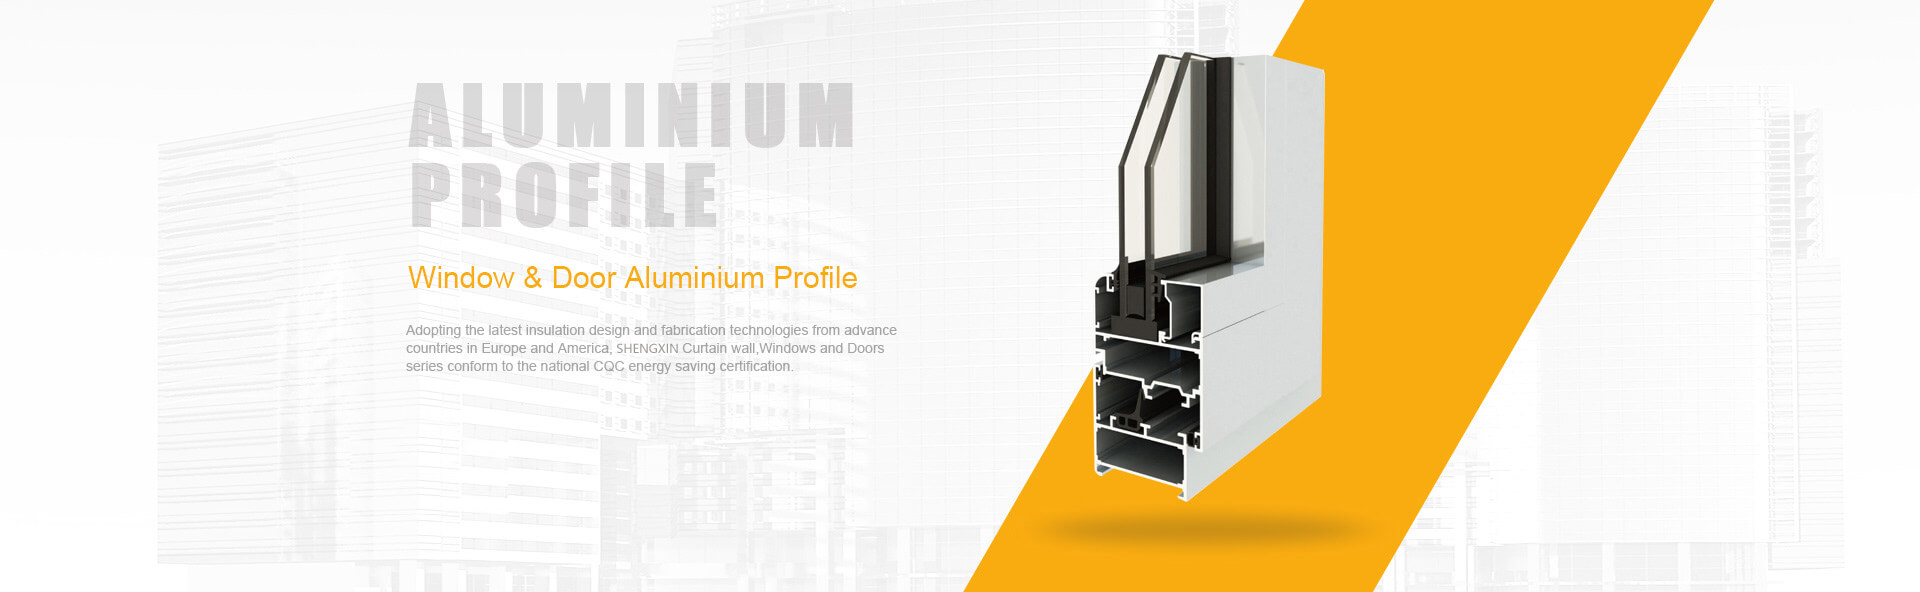
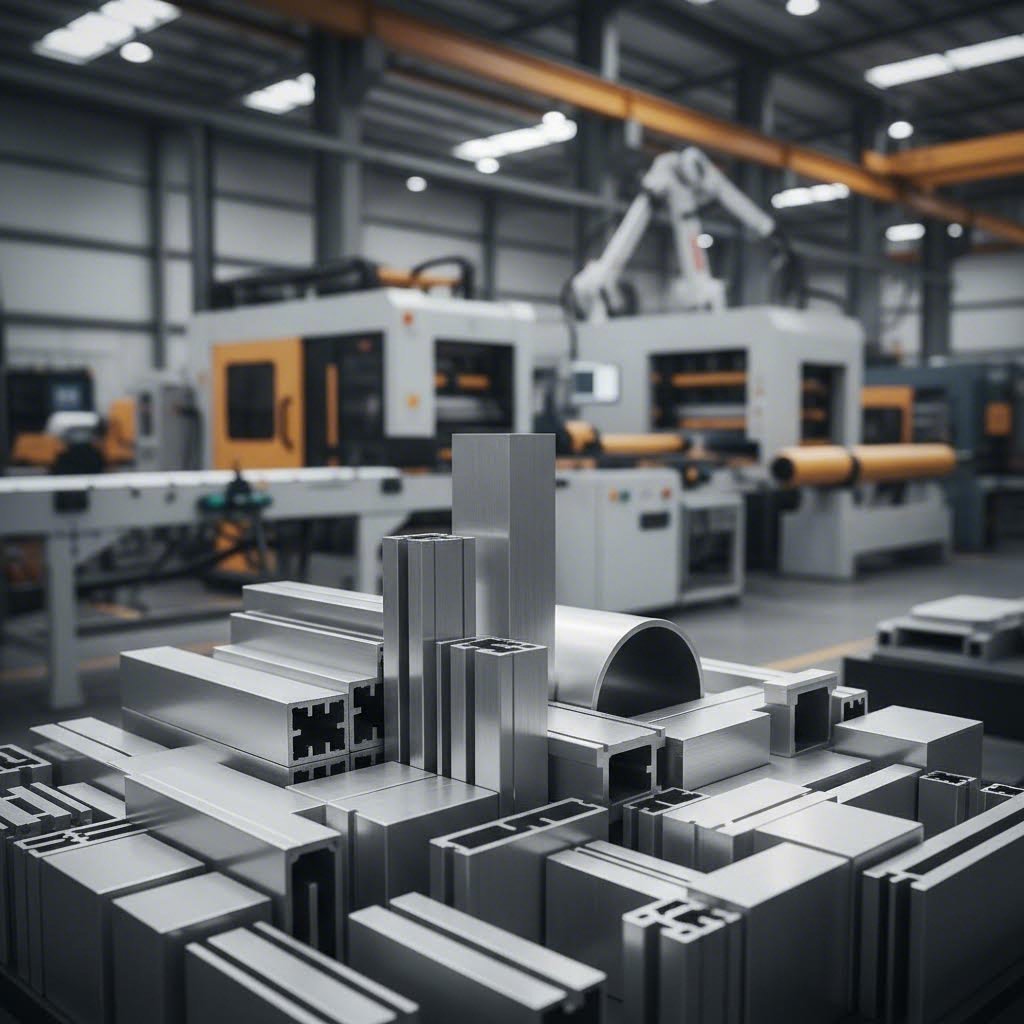
What is aluminum extrusion? Simply put, it's a manufacturing process that transforms aluminum alloy into shapes with specific cross-sectional profiles by forcing heated material through a shaped die. This versatile technique produces everything from simple bars to complex architectural components used across countless industries.
Aluminum extrusions definition: Continuous lengths of aluminum alloy shaped by pushing heated billets through precision-engineered dies to create uniform cross-sectional profiles for structural, decorative, and functional applications.
When you're searching for the right profile for your project, understanding the different types of aluminum extrusions becomes essential. However, terminology can get confusing fast. Are we talking about how the extrusion is made, what shape it takes, or how it's configured internally? These three categories—process types, profile shapes, and configurations—represent distinct classification systems that affect your final product in different ways.
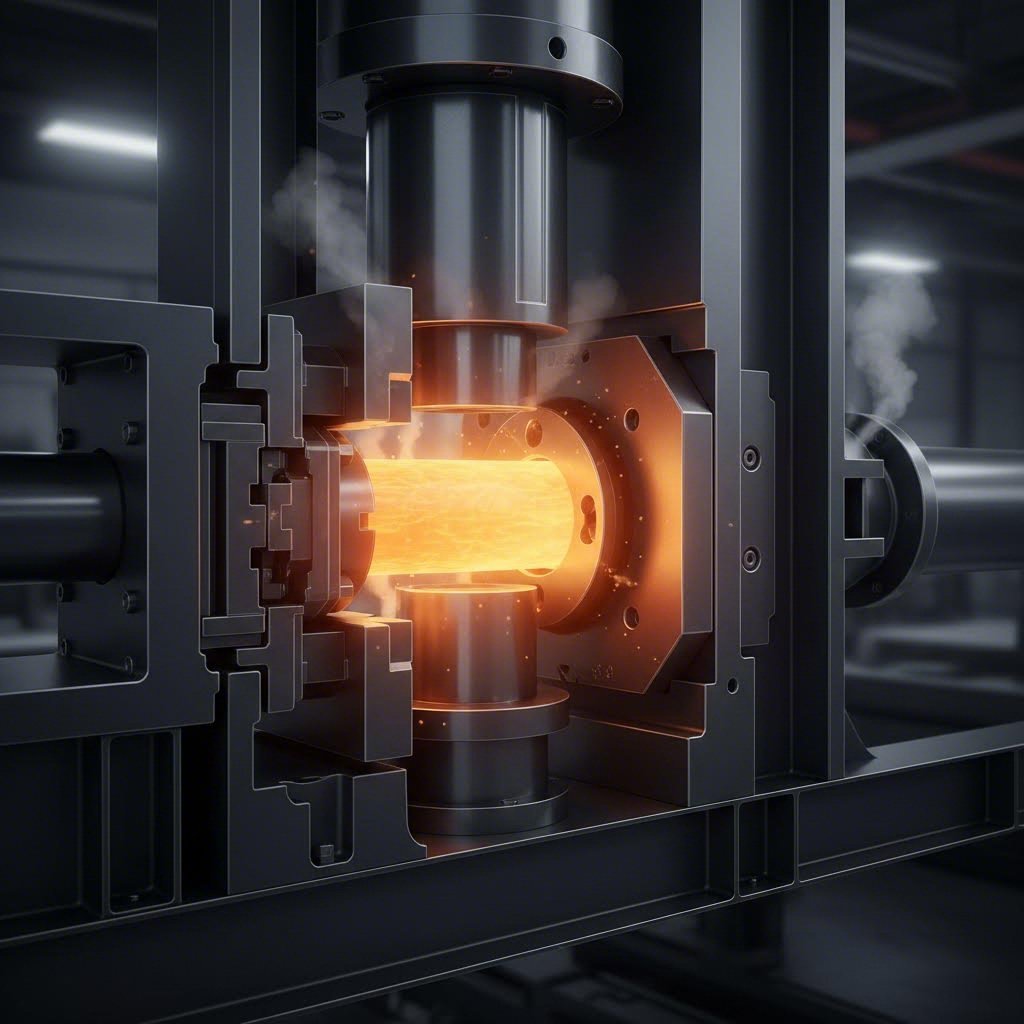
Imagine squeezing toothpaste through a tube—that's the basic concept behind what is extruded aluminum. A cylindrical aluminum billet gets heated until it becomes malleable, then a powerful hydraulic ram pushes it through a steel die with a precisely cut opening. The aluminum emerges on the other side with the exact cross-sectional shape of that die opening.
Here's why this matters for your specification process:
The aluminium extrusion definition extends beyond just the process—it encompasses the finished product itself. When someone asks "what is extrusions," they're often referring to both the manufacturing method and the resulting shaped aluminum lengths ready for fabrication.
You might wonder why aluminum has become the go-to material for extrusion applications. The answer lies in its unique combination of properties that make the definition of extruded aluminum practically synonymous with design flexibility.
Aluminum's relatively low melting point means it can be extruded at temperatures that don't destroy steel dies quickly. Its natural corrosion resistance eliminates the need for protective coatings in many applications. The material's excellent strength-to-weight ratio makes it ideal for transportation and construction where every pound matters.
Perhaps most importantly, aluminum extrusion allows designers to consolidate multiple parts into single profiles. A shape that might require welding, bolting, or assembling several steel components can often be extruded as one continuous aluminum piece—reducing labor, improving consistency, and cutting costs.
Understanding these fundamentals prepares you to navigate the specific categories ahead: hot versus cold processing methods, solid versus hollow configurations, and the wide variety of standard and custom profile shapes available for your application.
Now that you understand the fundamentals, let's explore how aluminum extrusion is made through three distinct temperature-based processes. Each aluminum extrusion process offers unique advantages depending on your project requirements, budget constraints, and desired final properties. Choosing the right method can mean the difference between a profile that exceeds expectations and one that falls short.
Hot extrusion stands as the most widely used aluminium extrusion process in the industry—and for good reason. This method heats aluminum billets above their recrystallization point, typically between 700°F and 930°F (375°C to 500°C), transforming the metal into a highly malleable state.
What does this mean for your project? When aluminum reaches these temperatures, it flows through the die with remarkable ease. According to Monroe Engineering, hot extrusion typically uses hydraulic presses capable of applying up to 100,000 pounds per square inch of pressure to the heated material. This combination of heat and pressure enables:
The trade-off? Hot extrusion produces surfaces with a slightly rougher finish compared to cold methods, and dimensional tolerances aren't quite as tight. However, for most architectural and structural applications, these characteristics fall well within acceptable ranges.
Sitting between hot and cold methods, warm extrusion offers a compelling middle ground that many engineers overlook. This extrusion aluminium process heats material to temperatures below the recrystallization point—roughly 800°F to 1,800°F depending on the specific alloy and application.
Why consider warm extrusion? You'll gain better surface finish than hot extrusion while maintaining more formability than cold processing. The reduced temperatures also extend die life compared to hot extrusion, translating to lower tooling costs over production runs.
Warm extrusion excels when you need:
When your application demands the tightest tolerances and best surface finish, aluminium cold extrusion delivers. This process forces aluminum through the die at or near room temperature, requiring significantly higher pressures but producing exceptional results.
Cold extrusion creates profiles with superior tensile strength because the process work-hardens the material as it's shaped. You'll notice smoother surfaces straight from the press, often requiring minimal secondary finishing. However, the geometric complexity you can achieve is more limited—the aluminum simply won't flow into intricate shapes without elevated temperatures.
This method works best for precision components in electronics, automotive, and aerospace applications where dimensional accuracy and surface quality justify higher processing costs.
| Characteristic | Hot Extrusion | Warm Extrusion | Cold Extrusion |
|---|---|---|---|
| Temperature Range | 700°F - 930°F (375°C - 500°C) | 800°F - 1,800°F (below recrystallization) | Room temperature to 300°F |
| Typical Applications | Architectural profiles, structural frames, complex shapes | Automotive components, moderate-precision parts | Precision parts, electronics housings, fasteners |
| Surface Finish Quality | Good (may require secondary finishing) | Very Good | Excellent (minimal finishing needed) |
| Dimensional Tolerances | Standard (±0.012" typical) | Improved (±0.008" typical) | Precision (±0.005" or better) |
| Relative Cost | Lowest | Moderate | Highest |
| Profile Complexity | High - intricate shapes possible | Moderate | Limited - simpler geometries only |
| Die Life | Shorter (heat stress) | Extended | Longest (no thermal stress) |
When selecting among these aluminum extrusion types, consider your priorities carefully. Need maximum design flexibility for complex profiles? Hot extrusion is your answer. Require precision parts with tight tolerances? Cold extrusion delivers. Looking for balanced performance at moderate cost? Warm extrusion might be the sweet spot.
Temperature selection in the extrusion extrusion process directly impacts everything from achievable geometries to final part strength. Understanding these relationships helps you specify the right process from the start—avoiding costly revisions and ensuring your profiles meet performance requirements.
With process methods covered, the next critical decision involves profile configuration: should your extrusion be solid, hollow, or semi-hollow? Each configuration brings distinct structural characteristics and cost implications to consider.
Beyond temperature-based processing methods, aluminum extrusion profiles fall into three fundamental configurations: solid, hollow, and semi-hollow. This classification determines not just what your finished part looks like, but also how complex the die must be, how fast production runs, and ultimately what you'll pay. Understanding these distinctions helps you match the right configuration to your structural requirements and budget.
According to Gabrian International, each configuration type has specific die and tooling requirements that directly impact manufacturability. Let's break down what makes each one unique—and when you should choose it.
Solid extruded aluminum profiles contain no enclosed voids or openings. Think of bars, angles, channels, and flat stock—shapes where aluminum fills the entire cross-section. These profiles represent the simplest extrusion shapes to manufacture because they require straightforward flat-face or pocket dies.
Why does simplicity matter? The die experiences uniform pressure distribution during extrusion, leading to longer die life and more consistent output. You'll typically see faster production speeds and lower tooling costs compared to hollow alternatives.
Solid aluminum extrusion shapes excel in applications requiring maximum strength-to-profile-size ratios. Structural framing members, heavy-duty brackets, mounting bars, and load-bearing components often specify solid configurations. When weight isn't your primary concern and mechanical performance is paramount, solid profiles deliver.
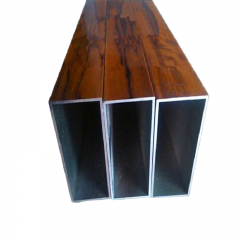
Hollow extruded aluminum shapes feature one or more fully enclosed voids—rectangular tubes, round pipes, and complex multi-void T-slot profiles all fall into this category. These configurations require porthole dies made up of two interlocking pieces: a mandrel that forms internal features and a cap that shapes external surfaces.
The manufacturing complexity increases significantly. Hot aluminum must flow around the mandrel's support legs, then reweld together before exiting the die. This welding process demands precise temperature control and adds processing considerations that affect both quality and cost.
When does weight savings justify hollow designs? Transportation applications where every gram matters, architectural curtain walls requiring thermal breaks, and modular framing systems demanding internal fastening channels all benefit from hollow configurations. The increased die cost pays off when you're producing sufficient volume or when the weight reduction provides measurable value.
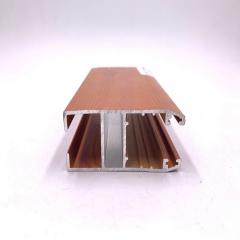
Semi-hollow aluminum extruded shapes occupy the middle ground—they have voids, but those voids aren't fully enclosed. Picture a narrow channel or a profile with deep grooves that nearly close but maintain an opening. This creates a manufacturing challenge that requires special consideration.
Here's where the tongue ratio concept becomes critical. As Gabrian's die engineering resources explain, the tongue ratio formula (Area/Gap²) determines whether a shape qualifies as semi-hollow. The larger the void area and the narrower the gap, the higher the tongue ratio—and the more difficult the extrusion becomes.
Why does this matter for your project? High tongue ratios mean the die's tongue area experiences concentrated stress during extrusion. The material wants to push that unsupported section, potentially causing breakage or deformation. Die designers must add complexity to strengthen these vulnerable areas, increasing tooling costs and potentially limiting achievable geometries.
Semi-hollow profiles work well for applications requiring partial enclosures—heat sinks with deep fin channels, grip handles with finger grooves, or decorative trim with shadow lines. Understanding tongue ratio limitations early in design prevents costly revisions when your manufacturer evaluates producibility.
Choosing between these configuration types ultimately comes down to balancing performance requirements against economics. Solid profiles cost less to tool but weigh more. Hollow profiles reduce weight but increase die investment. Semi-hollow configurations offer design flexibility but require careful attention to tongue ratios that affect both manufacturability and tooling longevity.
With configuration decisions clarified, the next consideration involves specific profile shapes—T-slots, angles, channels, tubes, and rails each serve distinct purposes across industries.
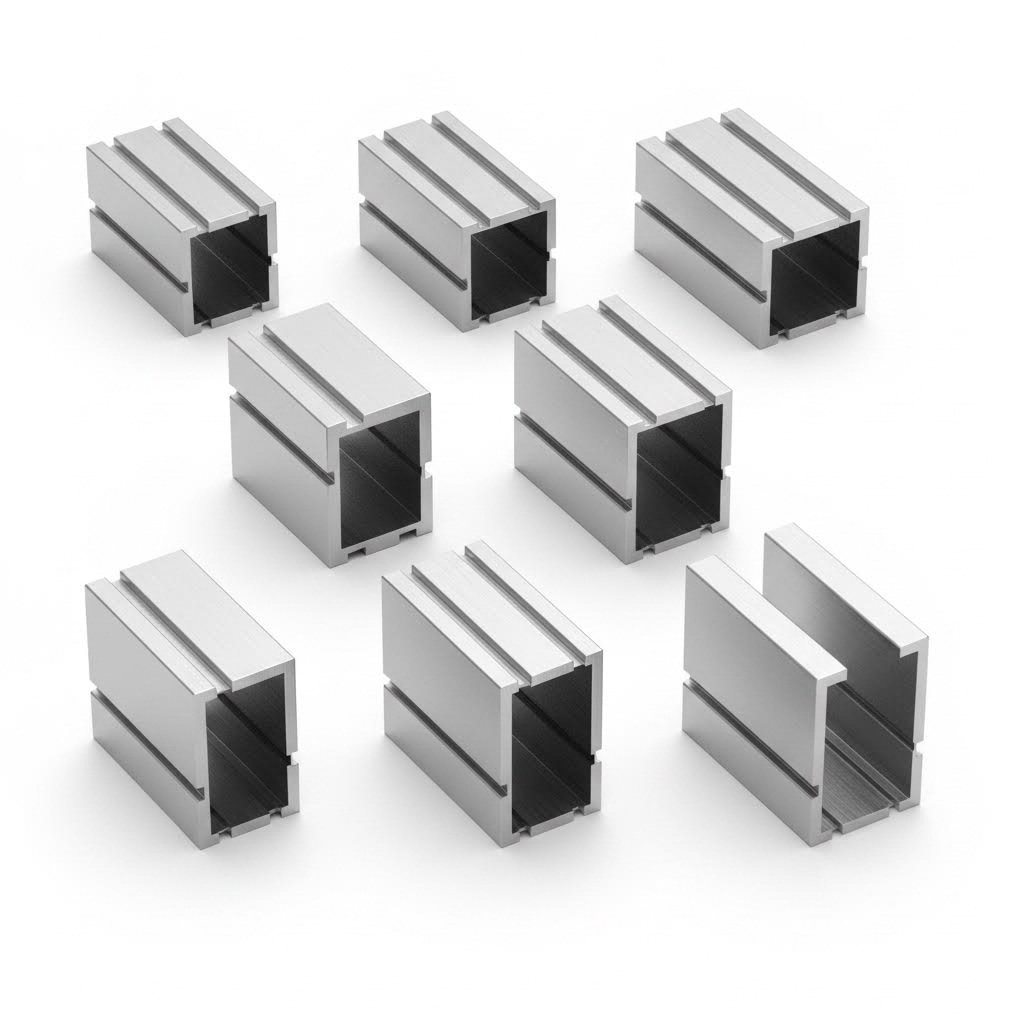
Now that you understand how configurations affect manufacturing complexity, let's explore the specific aluminum shapes available for your projects. Each aluminum profile type serves distinct structural and functional purposes—and knowing which shape fits your application saves time, reduces costs, and ensures optimal performance.
Standard aluminum profiles follow established dimensional series that ensure compatibility with connectors, fasteners, and accessories. According to Ya Ji Aluminum's profile sizing guide, the most common industrial sizes include the 20, 30, 40, 45, and 60 series—each corresponding to the base cross-sectional dimension in millimeters. This standardization means you can source compatible components from multiple suppliers without compatibility headaches.
| Profile Type | Typical Dimensions | Primary Applications | Structural Characteristics |
|---|---|---|---|
| T-Slot | 20×20mm to 80×160mm | Machine frames, workstations, automation systems | Modular assembly, high versatility, integrated fastening channels |
| Angle | Equal: 10×10mm to 100×100mm; Unequal: various | Corner bracing, trim, structural reinforcement | Excellent corner strength, simple fabrication, economical |
| Channel | 10mm to 200mm width; depths vary | Cable management, edge protection, sliding mechanisms | Open profile, easy access, good for routing and mounting |
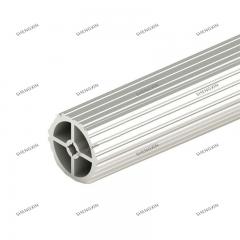
| Round Tube | 6mm to 300mm OD; wall 1-10mm | Handrails, furniture, hydraulic lines, structural supports | Uniform torsional strength, aesthetic appeal, pressure containment |
| Square/Rectangular Tube | 10×10mm to 200×200mm | Framework, equipment housings, conveyor systems | High rigidity, flat mounting surfaces, clean appearance |
| Bar (Flat/Round/Hex) | 3mm to 300mm diameter or width | Machined parts, brackets, spacers, shafts | Maximum material strength, easy to machine, solid construction |
| Rail | Custom profiles; 15-80mm typical height | Linear motion systems, drawer slides, curtain tracks | Precision surfaces, integrated bearing paths, low friction |
| Beam (I/H-Section) | 50mm to 300mm height | Structural frameworks, crane rails, heavy equipment | High moment of inertia, excellent load distribution, lightweight for strength |
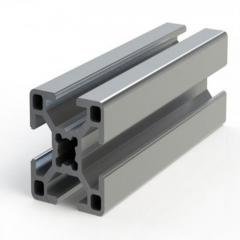
When should you choose slotted aluminum extrusion over simpler structural profiles? The answer depends on whether your project demands reconfigurability, rapid assembly, or future modification capability. T-slot aluminum profiles—sometimes called aluminum t profile systems—feature longitudinal grooves that accept T-nuts, bolts, and specialized connectors without drilling or welding.
The 40×40mm series profile stands as the most widely used industrial standard, balancing rigidity with weight. For lighter applications like lab equipment or 3D printer frames, 20×20mm profiles suffice. Heavy machinery and robotics typically require 60×60mm or larger sections.
Here's what makes T-slot systems uniquely valuable:
However, T-slot isn't always the right choice. When you need maximum structural efficiency and won't modify the assembly, welded tube or channel construction often costs less and weighs less. T-slot's versatility comes with material overhead—those grooves add cross-sectional area without adding proportional strength.
Industry applications for T-slot aluminum profiles span remarkably diverse sectors:
Sometimes the simplest aluminum shapes deliver exactly what your project needs. Angle profiles—L-shaped cross-sections with equal or unequal legs—provide corner reinforcement, edge protection, and economical structural support where T-slot complexity isn't warranted.
Standard angle dimensions range from small 10×10mm trim pieces to heavy 100×100mm structural members. Wall thickness typically varies from 1.5mm to 10mm depending on load requirements. Equal-leg angles work best for symmetrical applications, while unequal angles accommodate specific mounting or clearance needs.
Aluminum extrusion channel profiles offer open U-shaped or C-shaped cross-sections ideal for:
Both angle and channel profiles benefit from straightforward manufacturing. As solid extrusion shapes, they require simple flat-face dies that produce consistent results at competitive costs. When your application doesn't need enclosed voids or integrated fastening systems, these fundamental shapes often represent the most economical solution.
Hollow tube profiles—both round and square—combine structural efficiency with aesthetic appeal. The enclosed cross-section provides excellent resistance to bending and torsion while reducing weight compared to solid alternatives.
Round aluminum tubes excel in applications requiring:
Square and rectangular tubes offer different advantages. Their flat surfaces simplify mounting, alignment, and connection to other components. Framework applications benefit from the clean geometric appearance and straightforward joint fabrication.
Standard aluminum tube dimensions follow predictable progressions. Round tubes typically range from 6mm to 300mm outside diameter with wall thicknesses from 1mm to 10mm. Square tubes commonly span 10×10mm up to 200×200mm sections.
Aluminum extrusion rail profiles represent a specialized tube category designed for linear motion applications. These profiles feature precision surfaces—often V-grooves or flat tracks—that guide wheels, bearings, or sliding elements with minimal friction. You'll find them in:
According to Ya Ji Aluminum, V-slot rail systems have become particularly popular for robotics and 3D printer applications, allowing wheels or bearings to run directly along the grooves without separate rail hardware.
Selecting the right aluminum profile shape ultimately depends on matching structural requirements to available standard dimensions. Before specifying custom extrusions, explore whether standard aluminum profiles in the 20, 30, 40, 45, or 60 series meet your needs—established tooling means faster delivery and lower costs than custom die development.
With profile shapes understood, the next critical factor involves material selection. Different aluminum alloys dramatically affect extrudability, strength, surface finish, and corrosion resistance—making alloy choice inseparable from profile type decisions.
You've selected your profile shape and configuration—but which aluminum alloy should you specify? This decision dramatically impacts everything from how easily your profile extrudes to how it performs in service. Different types of aluminum offer distinct combinations of strength, workability, and surface finish quality that must align with your application requirements.
Among the common aluminum types used in extrusions, the 6xxx series dominates because these magnesium-silicon alloys deliver an exceptional balance of extrudability, strength, corrosion resistance, and weldability. However, within this series, significant differences exist that affect which profile types and applications each alloy serves best.
| Alloy | Extrudability Rating | Strength Characteristics | Surface Finish Quality | Recommended Profile Types |
|---|---|---|---|---|
| 6063 | Excellent (benchmark) | Medium strength (yield: 25-31 ksi) | Excellent - superior anodizing response | Thin-walled, complex architectural profiles, decorative trim |
| 6061 | Good (more difficult than 6063) | High strength (yield: 35-40 ksi) | Good - acceptable for most applications | Structural components, thick-walled profiles, machined parts |
| 6005/6005A | Very Good | Medium-high strength (between 6063 and 6061) | Very Good | Transportation, structural frames, ladder rails |
| 6082 | Good | High strength (comparable to 6061) | Good | Heavy structural applications, bridges, offshore platforms |
When surface appearance matters, 6063 aluminum stands as the undisputed choice among extruded aluminium alloys. According to Howard Precision Metals, this alloy's exceptional extrudability makes it ideal for thin-walled and architecturally sensitive applications where visual quality cannot be compromised.
What makes 6063 so special for extrusion? Its chemical composition—primarily alloyed with silicon and magnesium—creates material that flows smoothly through complex dies. This translates to:
You'll find 6063 aluminum extrusions in window frames, door systems, curtain wall mullions, furniture tubing, decorative trim, and automotive ornamental components. Whenever cosmetic appearance and surface treatment quality drive your specification, this alloy delivers.
What if your application demands more mechanical performance than 6063 provides? That's where 6061 aluminum enters the picture. As Howard Precision Metals notes, when material strength is the primary concern, 6061 becomes the optimal choice between these two widely used alloys.
The strength advantage comes from slightly different alloying elements—6061 contains additional copper and chromium that enhance its grain structure after heat treatment. This precipitation-hardened alloy offers approximately 30-40% higher yield strength than 6063 in comparable tempers.
Consider 6061 for aluminum extrusions requiring:
The trade-off? 6061 doesn't extrude as easily as 6063. Expect thicker minimum wall requirements, less intricate achievable geometries, and slightly rougher surface finishes. For applications where strength trumps aesthetics, these compromises are worthwhile.
Beyond the 6063/6061 comparison, different kinds of aluminum alloys address specialized requirements. The 6005 and 6082 alloys bridge the gap between extrudability and strength, while other series offer unique properties for specific applications.
6005/6005A: This alloy offers strength approaching 6061 with extrudability closer to 6063. Transportation industries favor it for railcar components, truck trailer frames, and ladder rails where both strength and reasonable profile complexity matter.
6082: Common in European markets, this high-strength alloy rivals 6061 performance. Heavy structural applications including bridges, crane components, and offshore platforms specify 6082 when maximum mechanical properties are essential.
Understanding temper designations proves equally important when specifying types of aluminium for extrusion. The temper code following the alloy number indicates the thermal and mechanical processing that determines final properties:
A complete specification reads like "6063-T5" or "6061-T6"—indicating both alloy composition and heat treatment condition. The T5 temper suits most architectural 6063 applications, while T6 delivers maximum performance from structural alloys.
How do you balance extrudability against mechanical requirements? Start with your non-negotiable performance criteria. If surface finish quality and complex thin-walled profiles define success, 6063 is your answer. If structural calculations demand specific yield strength values, work backward from those requirements to identify suitable alloys. When both factors matter, 6005 or 6005A often provides the optimal compromise.
With alloy selection clarified, another critical consideration awaits: how will your profiles manage heat? Thermal management extrusions require specific design principles that affect both profile geometry and material performance.
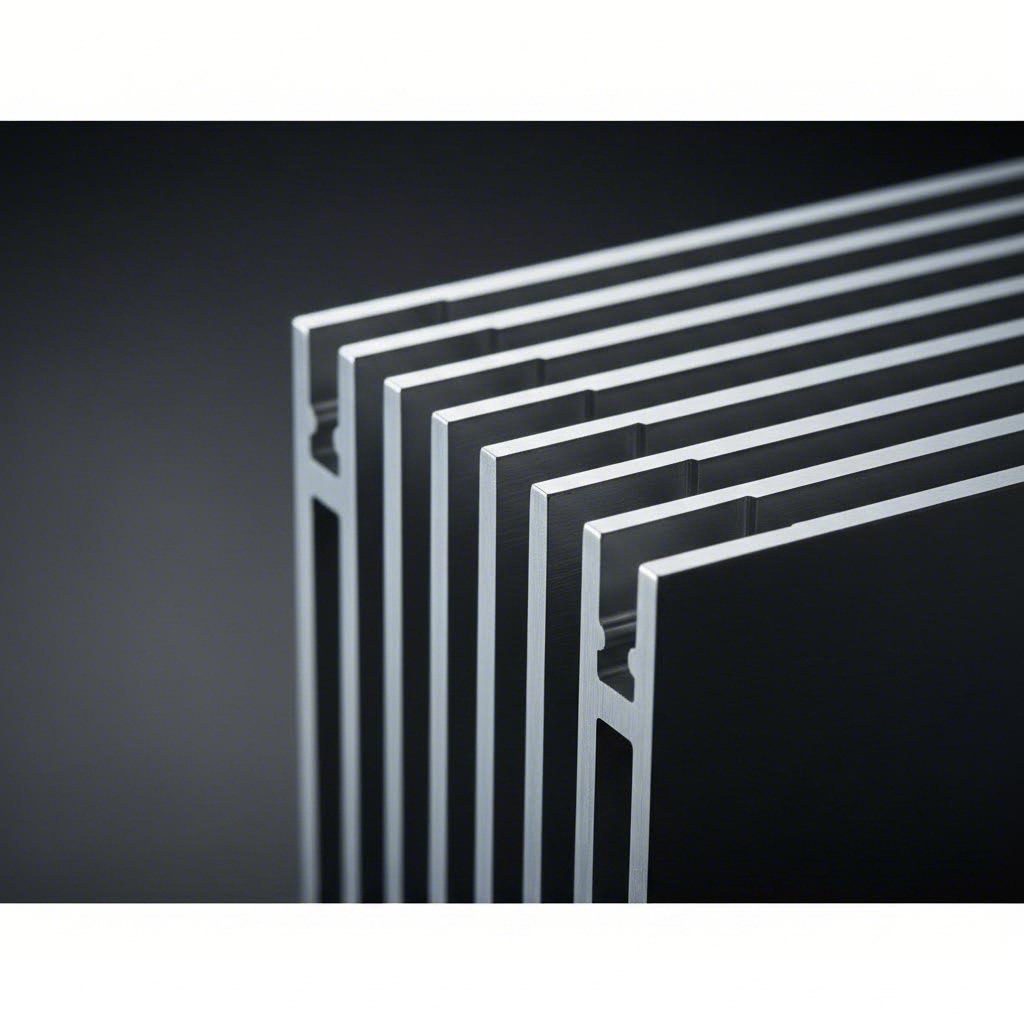
When your application generates heat—whether from LEDs, power electronics, or industrial equipment—standard aluminum extrusion profiles won't cut it. Thermal management extrusions represent a specialized category where profile geometry directly determines cooling performance. Understanding how fin design, base thickness, and surface area interact helps you specify the right aluminum extrusion profile for your thermal load requirements.
Why does aluminum dominate heatsink applications? The answer lies in its thermal conductivity (approximately 205 W/m·K for 6063 alloy), combined with the extrusion process's ability to create complex fin geometries in a single operation. Unlike machined or bonded heatsinks, extruded aluminium profiles offer cost-effective solutions for high-volume thermal management needs.
Designing effective thermal extrusion profiles requires balancing heat transfer physics against manufacturing constraints. Every heatsink must accomplish three things: absorb heat from the source, conduct it through the base, and dissipate it into the surrounding air via the fins.
Here are the key design considerations that determine thermal performance:
How does the extrusion process limit achievable geometries? Fin thickness, height, and spacing all face practical constraints. Most extruders can produce fins as thin as 1.0-1.5mm, but thinner sections become difficult to fill consistently. Fin heights typically max out around 8-10 times the gap width for natural convection designs—beyond this ratio, die tongue stress becomes problematic.
Sounds complex? Think of fin density selection as finding the sweet spot between surface area and airflow. Pack fins too tightly, and air can't flow between them. Space them too widely, and you're wasting potential cooling capacity.
For natural convection cooling—where no fans force air movement—optimal fin spacing typically ranges from 6mm to 12mm depending on fin height. The buoyancy-driven airflow needs room to develop. Cramming more fins into the same width actually reduces cooling performance because stagnant air trapped between closely-spaced fins acts as an insulator.
Forced convection changes the equation. With fans or blowers moving air across the heatsink, tighter fin spacing (3-6mm) becomes viable. The increased air velocity overcomes flow resistance, and the additional surface area translates directly to improved heat dissipation.
Consider these guidelines when selecting extrusion profiles for thermal applications:
Die complexity directly impacts heatsink extrusion costs. Simple profiles with 6-8 widely-spaced fins require straightforward tooling. High-fin-count designs with tight spacing demand precision dies that cost more to manufacture and maintain. When specifying thermal extrusion profiles, balance cooling requirements against tooling economics—especially for lower-volume applications where die costs represent a significant percentage of total project expense.
Where do you encounter high-performance aluminum extrusions industrial applications for thermal management? LED lighting and power electronics represent two of the fastest-growing sectors driving demand for specialized heatsink profiles.
LED lighting applications require consistent thermal management to maintain light output and extend fixture life. LEDs convert only 30-40% of input power to light—the rest becomes heat that must be dissipated. Common aluminum extrusion applications include:
Power electronics cooling presents different challenges. IGBTs, MOSFETs, and power modules generate concentrated heat loads that demand efficient spreading and dissipation. Aluminum extrusion profile designs for these applications often feature:
Industrial equipment cooling encompasses motor drives, power supplies, servo amplifiers, and control cabinets. These applications often specify modular heatsink profiles that can be cut to length and configured for specific thermal loads. Standard aluminium extrusion profile sections with pre-engineered fin geometries reduce design time and tooling investment.
When evaluating thermal extrusion options, remember that profile complexity affects more than just die cost. Complex heatsink geometries with high fin counts and tight tolerances typically extrude more slowly, require more frequent die maintenance, and may limit achievable lengths. For production applications, discuss thermal requirements with your extrusion partner early—they can often suggest profile modifications that improve manufacturability without compromising cooling performance.
With thermal management principles covered, the next consideration involves how surface treatments affect both appearance and performance of your finished extrusions.
Your aluminum extrusion profile is shaped, alloyed, and ready for production—but how will it look and perform in its final environment? Surface treatment selection determines not just appearance, but also corrosion resistance, wear characteristics, and dimensional accuracy of your finished aluminium extrusion. Choosing the right finish requires balancing aesthetic requirements against environmental demands and budget constraints.
Every aluminum extruded profile leaves the press with what's called a mill finish—the natural surface resulting from the extrusion process. For some industrial applications, this untreated surface works fine. But for most projects, secondary finishing transforms raw extrusions into components ready for demanding service conditions.
| Surface Treatment | Durability Rating | Color Options | Cost Level | Ideal Applications |
|---|---|---|---|---|
| Mill Finish | Low - susceptible to oxidation and marking | Natural aluminum (silver-gray) | Lowest (no treatment) | Hidden structural components, parts requiring machining |
| Anodizing (Clear) | High - excellent corrosion and wear resistance | Natural metallic appearance | Moderate | Architectural trim, consumer products, marine environments |
| Anodizing (Colored) | High - dyed colors may fade in UV exposure | Wide range including black, bronze, gold, blue, red | Moderate-High | Architectural facades, decorative applications, signage |
| Powder Coating | Very High - excellent impact and chemical resistance | Unlimited RAL and custom colors, textures available | Moderate | Outdoor furniture, window frames, industrial equipment |
| PVDF Coating | Exceptional - 20+ year exterior performance | Full color range with superior UV stability | High | Curtain walls, storefronts, high-rise architectural panels |
| Mechanical Finishing | Varies - depends on subsequent treatment | Brushed, polished, or textured metallic | Moderate | Decorative trim, appliances, consumer electronics |
What makes anodizing different from applied coatings? Rather than adding material to the surface, anodizing converts the aluminum itself into a hard aluminum oxide layer through an electrochemical process. This integral oxide becomes part of the aluminium extruded profile—it cannot peel, flake, or delaminate like applied finishes.
The anodizing process immerses your extrusion in an acid electrolyte bath while passing electrical current through it. Oxygen ions combine with aluminum atoms at the surface, building an oxide layer that's significantly harder than the base metal. Standard architectural anodizing produces oxide thicknesses of 15-25 microns, while hard anodizing can exceed 50 microns for extreme wear applications.
Why does this matter for your project? Consider these anodizing advantages:
However, anodizing adds thickness to your profile. Expect dimensional growth of approximately half the oxide thickness on each surface. A 20-micron anodize coating adds roughly 10 microns (0.0004") per side—critical to consider for precision-fit components. Specify tolerances accounting for anodize buildup, or request selective masking of critical surfaces.
When unlimited color options and maximum impact resistance matter more than metallic appearance, powder coating delivers. This dry finishing process applies electrostatically charged powder particles to grounded extruded metal, then cures the coating in an oven where particles fuse into a continuous film.
Powder coating offers distinct advantages over liquid paints:
Powder coating works exceptionally well for aluminum extrude profiles destined for outdoor furniture, playground equipment, architectural windows, and industrial enclosures. The thick, resilient coating shrugs off impacts that would chip or scratch thinner finishes.
The limitation? Powder coating is an applied finish that sits on top of the aluminum surface. While modern pretreatments create excellent adhesion, the coating can potentially chip or peel if severely damaged. For applications where the metallic character of aluminum matters—or where the finish must withstand decades of UV exposure without recoating—other options may serve better.
Some environments demand more than standard anodizing or powder coating can deliver. Architectural curtain walls on high-rise buildings, coastal installations, and industrial chemical processing all require specialized surface treatments matched to specific exposure conditions.
PVDF (Polyvinylidene Fluoride) Coatings: When your extrusion of aluminium faces decades of UV exposure, PVDF fluoropolymer coatings provide unmatched weathering performance. These high-performance liquid coatings—sold under trade names like Kynar 500 and Hylar 5000—maintain color stability and gloss retention for 20+ years in direct sunlight. Architectural specifications for curtain walls, storefronts, and building facades frequently mandate PVDF finishes.
Mechanical Finishing: Before coating, mechanical treatments modify surface texture and appearance:
Mechanical finishing often precedes anodizing or coating, with the texture preserved through subsequent treatment. A brushed and clear-anodized aluminum profile combines metallic character with durable protection.
How does finish selection affect dimensional tolerances? Every surface treatment adds material or modifies surfaces in ways that impact final dimensions:
For precision assemblies, specify finished dimensions rather than base profile dimensions, allowing your supplier to compensate during extrusion. Alternatively, mask critical surfaces or plan for post-finishing machining of tight-tolerance features.
Architectural versus industrial finish requirements differ significantly. Architectural aluminum demands consistent appearance across large visible surfaces, strict color matching between lots, and long-term aesthetic performance. Industrial applications typically prioritize functional protection—corrosion resistance, wear characteristics, and chemical compatibility—with appearance secondary.
Matching surface treatment to your application environment ensures your aluminum profiles perform as intended for their full service life. With finish options clarified, the next step involves understanding how different industries apply these profile types, configurations, and treatments to solve real-world engineering challenges.
How do all these profile types, configurations, alloys, and finishes come together in real-world applications? Each industry sector demands specific combinations tailored to unique performance requirements. Understanding which aluminum profile extrusion solutions work best for your sector helps you specify the right components from the start—avoiding costly mismatches between material capabilities and application demands.
From towering glass curtain walls to lightweight automotive structures and modular factory workstations, structural aluminum extrusions solve engineering challenges across remarkably diverse fields. Let's examine how major industries leverage different extrusion types to achieve their performance goals.
Walk past any modern commercial building, and you're looking at aluminum extrusions in action. Window frames, door systems, curtain wall mullions, and structural glazing components rely almost exclusively on extruded aluminum for their combination of strength, corrosion resistance, and design flexibility.
What makes aluminum ideal for architectural applications? The ability to integrate multiple functions into single extruded aluminum frame profiles eliminates assembly complexity while improving thermal and structural performance.
Typical architectural applications include:
For these applications, 6063-T5 alloy dominates due to its superior extrudability and excellent anodizing response. Architectural projects demand consistent surface appearance across hundreds of visible profiles—6063's smooth extrusion characteristics deliver that consistency.
Surface finish selection varies by exposure and aesthetic requirements. Interior applications often use clear or bronze anodizing. Exterior curtain walls typically specify PVDF coatings for decades of color stability. Powder coating serves mid-range applications where cost considerations balance against performance needs.
Every kilogram removed from a vehicle improves fuel efficiency and reduces emissions. Automotive engineers increasingly specify extruded structural aluminum to replace heavier steel components—achieving weight reductions of 40-50% while maintaining or improving crash performance.
The aluminum extrusion tube has become particularly important for automotive applications. Hollow profiles provide excellent energy absorption during collisions, crushing progressively to protect occupants while minimizing vehicle mass.
Key automotive and transportation applications include:
Alloy selection shifts toward higher-strength options for transportation. While 6063 handles decorative trim, structural components typically require 6061-T6 or 6005A for their superior mechanical properties. These alloys provide the yield strength necessary for crash energy management calculations.
Rail and mass transit applications extend these principles to larger scales. Train car body structures, interior framing, and seating systems all leverage aluminum's weight advantages. Structural aluminium extrusions in these applications often feature complex hollow configurations optimized for specific load paths.
Step into any modern manufacturing facility, and you'll find T-slot aluminum framing everywhere. Machine guarding, conveyor systems, workstation structures, and robotic cell enclosures all rely on modular aluminum frame extrusions for their unmatched flexibility and rapid assembly.
Why has industrial automation embraced extruded aluminum so completely? The answer lies in reconfigurability. Production requirements change constantly—new products, updated processes, and evolving safety standards demand infrastructure that adapts without complete replacement.
Industrial automation applications include:
The 40×40mm T-slot profile serves as the industrial workhorse—strong enough for most applications while remaining easy to handle and cut. Heavier loads demand 60×60mm or 80×80mm sections, while light-duty applications like 3D printer frames work well with 20×20mm profiles.
For industrial environments, 6063-T5 provides adequate strength for most framing applications. Critical structural members or applications with higher load requirements may specify 6061-T6 for its enhanced mechanical properties. Surface treatments typically include clear anodizing for corrosion protection in general manufacturing or powder coating for environments with chemical exposure or aesthetic requirements.
Matching profile selection to specific industry requirements ensures optimal performance while controlling costs. Standard profiles serve the vast majority of applications—but knowing when custom extrusions justify their additional investment can unlock design possibilities that standard shapes simply cannot achieve.
You've identified the profile shape, configuration, alloy, and finish your project requires—but now comes a critical procurement decision. Should you source stock aluminum extrusion profiles from an existing catalog, or invest in custom tooling for a purpose-built design? This choice affects everything from initial costs to production timelines and long-term economics.
Many engineers default to custom extrusions when standard shapes would serve equally well. Others force-fit standard profiles into applications demanding specialized geometry, creating assembly complexity that erases any savings. Understanding when each approach makes sense helps you optimize both performance and budget.
| Factor | Standard Stock Profiles | Custom Extrusions |
|---|---|---|
| Tooling Cost | None - existing dies available | $500 - $5,000+ depending on complexity |
| Lead Time | Days to 2-3 weeks from stock | 4-8 weeks including die development |
| Minimum Quantities | Often 1-10 pieces from distributors | Typically 500-2,000 lbs per order |
| Design Flexibility | Limited to aluminum extrusion profiles catalog offerings | Unlimited within process constraints |
| Unit Cost (High Volume) | Moderate - includes distributor margins | Lower - factory-direct pricing possible |
| Part Consolidation | May require multiple profiles + assembly | Single profile can integrate multiple functions |
| Dimensional Optimization | Standard aluminum extrusion dimensions only | Exact specifications for your application |
When does custom extrusion make financial sense? The answer depends on volume, complexity, and how well standard aluminum extrusions match your requirements.
Imagine you need 100 pieces of a simple rectangular tube. Standard stock profiles ship within days at competitive per-piece pricing. Custom tooling would add $1,000-2,000 to your project cost, spread across only 100 units—that's $10-20 per piece just for die amortization before material costs even begin.
Now consider a different scenario: you're producing 10,000 window frame sections annually. A custom profile consolidating three separate standard shapes into one integrated extrusion eliminates two assembly operations per unit. Even with $3,000 die investment, the per-piece tooling cost drops to $0.30—and assembly savings of $2-5 per unit generate substantial returns.
Here's a framework for evaluating the economics:
Don't forget secondary operations in your calculations. A custom profile with integrated mounting features might cost more per pound than standard stock, but eliminating drilling, tapping, and bracket attachment often tips the economics toward custom—even at moderate volumes.
Profile complexity directly determines die cost and development timeline. Understanding these relationships helps you design manufacturable profiles that balance capability against tooling investment.
Simple solid profiles—bars, angles, and basic channels—require straightforward flat-face dies costing $500-1,500. These tools produce consistent results with minimal maintenance and long service life. If your application works with these shapes, tooling represents a minor investment.
Hollow profiles demand porthole dies with mandrels and caps working together to form internal voids. Expect tooling costs of $1,500-3,500 for typical hollow sections. Complex multi-void profiles—like elaborate T-slot configurations—can push die costs toward $5,000 or higher.
Several factors drive aluminum extrusion manufacturing die costs upward:
Working with experienced manufacturers early in design prevents costly surprises. A small radius change or wall thickness adjustment often reduces die complexity substantially without affecting functional performance. Aluminum extrusion design guidelines from your supplier can identify optimization opportunities before tooling commitment.
Experienced manufacturers like Shengxin Aluminium provide end-to-end support from die development through mass production. With 35 extrusion presses ranging from 600T to 5500T capacity, they can match your profile requirements to appropriate equipment—ensuring optimal die performance and production efficiency regardless of profile complexity.
Production timelines vary dramatically between standard and custom extrusions. Planning appropriately prevents project delays that cost far more than any material premiums.
Standard aluminum extrusion profiles from distributor stock often ship within 3-5 business days. Even made-to-order standard shapes typically deliver in 2-3 weeks since dies already exist. This speed suits prototype development, small production runs, and urgent replacement needs.
Custom extrusions follow a longer path:
Total lead time from order to delivery typically runs 4-8 weeks for custom profiles. Complex dies or tight tolerance requirements can extend this timeline. Build these realities into project schedules—last-minute custom extrusion orders rarely end well.
Minimum order quantities present another planning consideration. Standard stock profiles sell in small quantities—sometimes single pieces for prototyping. Custom extrusions carry minimums driven by production economics:
Typical custom extrusion minimums range from 500-2,000 pounds per order, though some manufacturers accommodate smaller quantities for premium pricing. If your annual usage falls below these thresholds, evaluate whether standard profile adaptation costs less than custom extrusion premiums.
Common selection mistakes to avoid:
The right choice depends on your specific situation. When standard aluminum extrusions from an aluminum extrusion dimensions catalog meet requirements, they deliver speed and flexibility. When performance optimization, part consolidation, or volume economics favor custom profiles, the die investment pays dividends across production life.
With procurement strategy clarified, the final step involves pulling together all these selection criteria into an actionable specification process that ensures you get exactly the right extrusion for your application.
You've explored process methods, profile configurations, alloy options, surface treatments, and industry applications—but how do you translate all this knowledge into an actionable specification? Selecting the right types of aluminum extrusion requires systematically evaluating your project requirements against available options. Let's distill everything into a practical framework you can apply immediately.
Understanding what is aluminum profile selection really comes down to matching four interconnected decisions: extrusion type (hot, warm, or cold processing), profile configuration (solid, hollow, or semi-hollow), alloy grade (6063, 6061, or specialty options), and surface treatment (anodizing, powder coating, or other finishes). Each choice affects the others—and getting them right from the start prevents costly revisions downstream.
Ready to specify your aluminum extrusions? Work through this systematic checklist to ensure you've addressed every critical factor before contacting suppliers:
Working through each item systematically prevents the common mistake of optimizing one factor while overlooking others. A profile with perfect mechanical properties means nothing if the surface treatment fails in your environment—or if tooling costs exceed your entire project budget.
What are aluminum extrusions used for in your specific application? The answer shapes everything from initial consultation through final delivery. Experienced extrusion partners do more than simply fill orders—they help optimize your specifications for manufacturability, performance, and cost.
When evaluating potential suppliers, consider their capabilities across the full production spectrum. Can they handle both types of extruded aluminum you might need—from simple standard shapes to complex custom profiles? Do they offer the surface treatments your application demands? What's their track record with similar applications in your industry?
Here's what to look for in a comprehensive extrusion partner:
The relationship between extrusion type, configuration, alloy, and surface treatment forms an integrated system. Changing one element often affects optimal choices for others. A partner who understands these interdependencies helps you navigate trade-offs rather than simply accepting whatever specifications you provide.
For projects requiring comprehensive aluminum extrusion solutions, Shengxin Aluminium offers complete capabilities from custom 6063 aluminum tubes to complex industrial profiles. Their 35 advanced extrusion presses—ranging from 600T to 5500T capacity—enable diverse profile capabilities matched to specific project requirements. Surface treatment options include anodizing in custom colors like Champagne and Rose Gold, powder coating, PVDF, and micro-arc oxidation for superior durability.
What sets comprehensive partners apart? End-to-end support from die development through mass production, backed by technical teams who understand both manufacturing constraints and application requirements. Factory-direct pricing eliminates intermediary markups, while CNC machining centers provide precise cutting, drilling, and bending to your exact specifications.
Whether you're specifying types of aluminum extrusion for architectural facades, automotive components, or industrial automation systems, the selection process follows the same fundamental logic: define requirements, evaluate options, optimize trade-offs, and partner with manufacturers who can execute your vision. Start with the checklist above, engage with knowledgeable suppliers early, and you'll match the right profile to your project every time.
The three main types of aluminum extrusion profiles are solid, hollow, and semi-hollow configurations. Solid profiles contain no internal voids and offer maximum structural integrity with simpler die designs. Hollow profiles feature fully enclosed voids like tubes and provide excellent weight-to-strength ratios. Semi-hollow profiles have partially enclosed voids and require careful attention to tongue ratios during manufacturing. Each type suits different applications based on structural requirements, weight considerations, and budget constraints.
The primary difference lies in extrudability versus strength. 6063 aluminum offers excellent extrudability, superior surface finish quality, and outstanding anodizing response, making it ideal for thin-walled architectural profiles and decorative applications. 6061 aluminum provides approximately 30-40% higher yield strength but is more difficult to extrude. Choose 6063-T5 for window frames and aesthetic components, and 6061-T6 for structural load-bearing applications like automotive chassis parts and aircraft components.
Aluminum extrusions serve countless applications across industries. In architecture, they form window frames, door systems, and curtain wall mullions. Automotive applications include crash management systems and structural frame rails. Industrial uses encompass T-slot machine guarding, conveyor frameworks, and workstation structures. Additional applications include heatsinks for electronics cooling, LED lighting housings, furniture tubing, and modular construction systems. Their versatility comes from combining strength, corrosion resistance, and design flexibility.
Consider volume, complexity, and cost trade-offs. Standard profiles work best for low volumes under 500 lbs, offering quick delivery with no tooling investment. Custom extrusions justify their $500-5,000+ die costs when annual volumes exceed 5,000 lbs or when part consolidation eliminates multiple assembly operations. Partners like Shengxin Aluminium provide technical support from die development through mass production, with 35 extrusion presses ranging from 600T to 5500T capacity for diverse profile requirements.
Common surface finishes include mill finish (natural untreated surface), anodizing (creates integral oxide layer for corrosion resistance and color options), powder coating (offers unlimited colors with excellent impact resistance), and PVDF coatings (provides 20+ year exterior weathering performance). Mechanical finishes like brushing and polishing modify surface texture before coating. Selection depends on environmental exposure, aesthetic requirements, and durability needs. Each treatment affects final dimensions differently.


 online service
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 English
 français
 Deutsch
 русский
 español
 português
 العربية
 ไทย
 Việt
 Українська