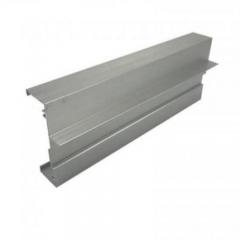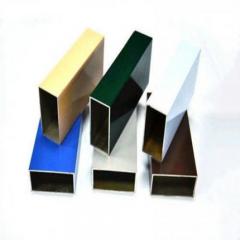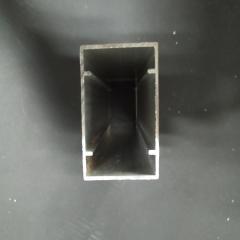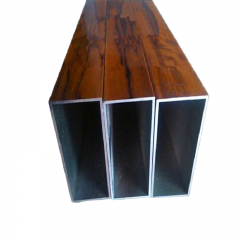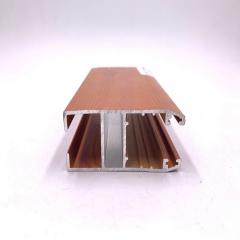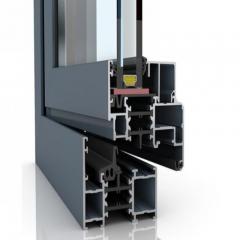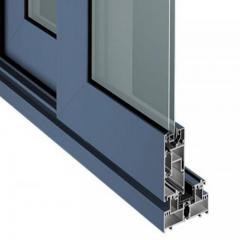
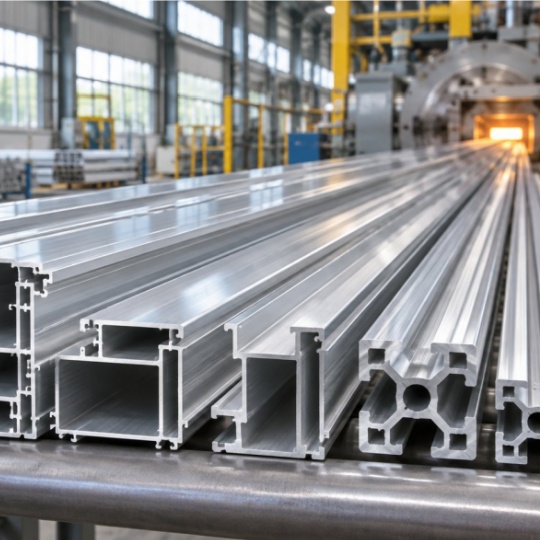
6063 Aluminum Extrusion: Specify The Right Temper Before You Order What 6063 Aluminum Extrusion Is and Why It Matters 6063 aluminum is a wrought aluminum-magnesium-silicon alloy in the 6xxx series, registered with the Aluminum Association. Extruders choose it because it flows easily through a die into complex shapes and leaves a smooth surface that anodizes well, which makes 6063 aluminum extrusion a common choice for window frames, trim, tubing and heat sinks. What Is 6063 Extrusion Aluminum The name comes from the Aluminum Association's four-digit system for wrought alloys, published in its Teal Sheets. The first digit, 6, puts the alloy in the series whose main additions are magnesium and silicon. The second digit, 0, means this is the original alloy and not a later modification. The last two digits, 63, identify this particular alloy within the 6xxx family. Magnesium and silicon are the reason the alloy can be heat treated. During aging, they combine into very fine particles of magnesium silicide (Mg2Si), which make the metal harder to deform and raise its strength. Extrusion is the shaping step. Every aluminum 6063 extrusion starts as a heated billet that a press pushes through a steel die cut to the profile's outline, a bit like squeezing toothpaste from a tube. The metal comes out as a long length with the same cross-section all the way along. Why 6063 Is Known as the Architectural Alloy Look at a storefront frame or a sliding door track and you'll notice clean edges and an even, bright surface. That appearance is the main reason the alloy is often called architectural aluminum. 6063 has a low impurity content and a smooth surface straight off the press, so it builds a uniform anodized layer. Clear and colored finishes therefore look consistent from one length to the next. The trade-off is strength. 6063 sits at the moderate end of the 6xxx series and is weaker than 6061, so it fits frames, trim and light structures better than heavy load-bearing parts. Where 6063 Aluminum Extrusions Are Used Window and door frames, including curtain wall systems Roofing components and architectural trim Sign frames and display structures Round, square and rectangular tubing T-slot framing for workstations and machine guards Heat sinks, where the alloy's thermal conductivity matters: 6063-T6 conducts about 201 W/m-K, compared with about 167 W/m-K for 6061-T6, and published values for 6063 in T5 and T6 run from roughly 200 to 218 W/m-K. Because the alloy flows easily, it can also be extruded into thin fins. All of these uses depend on a tightly limited chemistry, so the guide starts with composition and then covers tempers, properties, the extrusion process, profile design, finishing and sourcing. 6063 Composition and How It Compares With 6061 Why does one alloy slide easily through a die while a close relative resists? The difference comes from a few tenths of a percent of magnesium, silicon and copper. The Aluminum Association sets these limits in its reg...
Read More
How to Choose an Aluminum Extrusion Manufacturer and Own Your Dies Step 1. Qualify Your Part Before You Search for Suppliers To choose an aluminum extrusion manufacturer, start by writing down the part, before you look at any supplier list. The alloy, size, tolerances, finish and volume decide which manufacturers can make the part at all, so a clear spec cuts a long search down to a short one. Imagine sending a rough sketch to ten extruders and getting three replies, each quoting a different alloy and length. That spread usually means the request left too much open. Profile Precision Extrusions makes the point in its extrusion design guide that circle size and alloy set the first limits on what a shop can produce. The sections below expand that idea into a full spec you can complete before you search. Define Alloy, Temper and Profile Envelope Most custom profiles use 6000-series alloys. A 6061 vs. 6063 vs. 6005 comparison from Metra describes 6063 as the choice for fine detail and anodized or painted surfaces, 6061 for heavy structural loads and machining, and 6005A as a middle option with close to 6061 strength and better extrudability. Record the temper as well, such as T5 or T6, because it sets the final mechanical properties. If your part is window trim or a lighting track, a 6063 aluminum extrusion manufacturer is a natural place to start. If you specify a 2000- or 7000-series hard alloy, expect far fewer suppliers. Alloys such as 2024 and 7075 need specialized processing and heat treatment, and many extruders don't offer it. Next, record the profile envelope: Circumscribing circle diameter (CCD): the smallest circle that fully encloses the cross-section. Minimum wall thickness and weight per foot. Geometry type: solid, semi-hollow or hollow. Cut length of the finished piece. These numbers rule suppliers out because of how the aluminum extrusion manufacturing process works. A heated billet is pushed through a steel die, and the profile is then quenched, aged and cut to length. The press and die have to accommodate the CCD. Thin walls need a die that keeps metal flow balanced, and hollow profiles need more complex dies. Quenching also varies by alloy: 6063 can be air-quenched on the runout table, while 6061 often needs a water quench that can distort the profile without careful control. As one example of a published limit, PPE's guidance covers profiles that fit within roughly a 3.5 to 4.0 inch circle, with a 0.025 in. minimum wall for 6063. A buyer looking for a lightweight aluminum extrusion manufacturer for thin-walled parts can screen shops quickly against published figures like these. PPE notes that its figures are design guidelines, so final feasibility is still confirmed on the actual drawing. Set Tolerances, Finish and Secondary Operations Name the tolerance standard that applies to your part: US buyers: ANSI H35.2 or ASTM B221 European buyers: EN 755-9 Chinese mills: GB/T 14846 Then mark only the critical-to-quality dimensions as tig...
Read More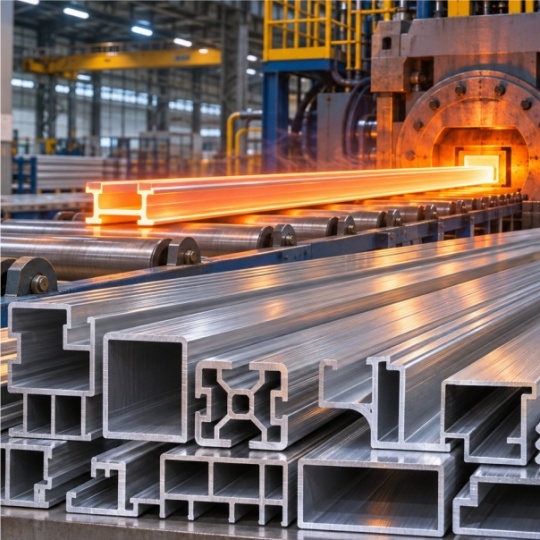
Skip The Rankings: Vet An Aluminium Extrusion Company On Specs What an Aluminium Extrusion Company Does and Why the Supplier Type Matters What is an aluminium extrusion company? An aluminium extrusion company heats aluminium billets until they soften, then uses a hydraulic press to push them through a shaped steel die. The result is a continuous profile with a fixed cross-section, which the company cuts to length, heat-treats and often machines or finishes before shipping. A note on spelling: this guide uses "aluminium" as its main spelling, and "aluminum" is the US spelling. As the ANSI blog explains, both are correct, and the right one depends on who is reading. UK and US buyers are looking for the same parts. What an Aluminium Extrusion Company Actually Makes How can one press turn out both a plain angle and a window frame? The answer is the die. Tooling maker Gemini Group describes the die as a steel disk with a carefully designed opening, and that opening sets the cross-section of every profile pushed through it. If you change the opening, you change the product. Typical output runs from simple channels, angles, rod and bar to architectural frames, transportation and structural members, and fully custom shapes. Types of Aluminum Extrusion Companies and Who Each One Serves Search for an aluminium extrusion company and you'll notice that most of the pages near the top are written by vendors. Their "top supplier" lists tend to favor their own business model. A more useful question is which kind of supplier fits your part. Custom extruders run their own presses and dies. Pick one when you need a new profile shape or control over alloy, temper and tolerances. Distributors and metal service centers sell stock shapes from inventory. Pick one when a standard angle, tube or bar will do the job and speed matters. The Fabricator notes that service centers mostly provide general services such as warehousing and distribution to hundreds of industries. T-slot framing system vendors sell standard slotted profiles and connectors. They suit machine frames, guards and workstations that bolt together without custom tooling. Fabricators buy extrusions and then machine or assemble them. Choose this route when you want finished parts and the profile itself is standard or already sourced. This guide skips the rankings. It gives you vendor-neutral criteria instead: specs, standards and questions you can put to any supplier. The four supplier types differ mainly in how much of the aluminum extrusion chain each one controls, from the hot billet to the aged, cut-to-length profile. Following that chain step by step shows where your questions should start. How Extruded Aluminum Profiles Are Made From Billet to Finished Length Why might two suppliers quote very different lead times for the same drawing? The reason is usually in the process. Aluminum extrusion manufacturing follows much the same sequence at most plants, so once you know the steps, you can ask better quest...
Read More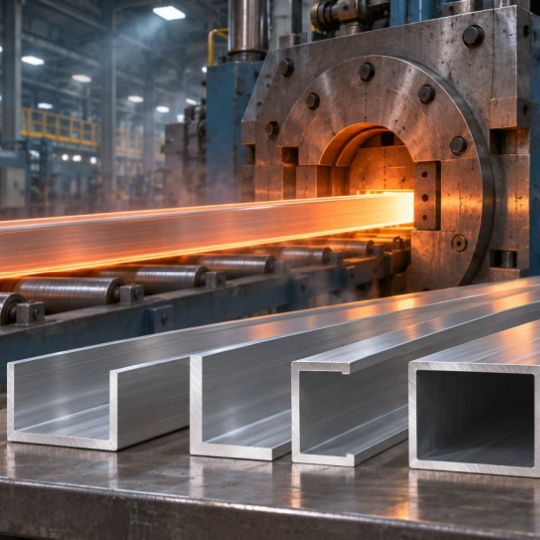
Custom Hard Alloy Extrusions: Why They Crack, Cost More And Run Late What Custom Hard Alloy Extrusions Are and Who Needs Them Custom hard alloy extrusions are profiles extruded to a buyer-specific cross-section from high-strength aluminum alloys, mainly the 2xxx and 7xxx series. These alloys are harder to push through a die than common 6xxx alloys, and that difficulty shapes the design limits, the price and the lead time. Have you ever sent a drawing to an extruder with 7075 called out and gotten back a quote far higher and slower than you expected? This guide explains why that happens. Hard alloy profiles go into parts where loads are high and weight is tight, such as wing spars, fuselage frames and other structures that take years of vibration and cyclic loading. Taber Extrusions notes that the 2xxx and 7xxx series provide the strength these parts need. The softer 6xxx alloys used in architectural and automotive work are not engineered for sustained high stress. What Hard Alloy Means in Aluminium Extrusion The term "hard alloy" has two meanings, and search results often mix them up. In aluminium extrusion, it means the high-strength 2xxx and 7xxx alloys. Some extruders also put high-magnesium 5xxx alloys in this group. In translated sources, "hard alloy" comes from the Chinese term yingzhi hejin and the Russian term tvyordy splav, and both mean cemented carbide, such as tungsten carbide. This article covers only the aluminum meaning. If you need extruded cemented carbide rods or preforms, you're looking for a separate product category with its own suppliers. How Custom Extrusions Differ From Standard Profiles A custom extrusion is a profile made from a die built for one buyer's drawing. A standard profile comes from a die that already sits in a manufacturer's library, so you can order it from a catalog. Profile Precision Extrusions sums up the trade-off. Catalog shapes ship fast and need no tooling, but the selection is limited and the tolerances are looser. Custom aluminum extrusions add a one-time die cost. In return, you get a cross-section designed around your part. Picture a frame rail that needs a mounting slot, a stiffening rib and a cable channel. Starting from a catalog shape, you would have to machine all of those features in. A custom die can extrude the whole cross-section directly. The Four Reference Alloys Used Throughout This Guide To keep the comparisons consistent, every later section rates aluminum extrusion profiles against the same four alloys: 6063: the easy-to-extrude baseline for speed, finish and design freedom. 6061: the general structural alloy, and usually the first one to consider before moving to a hard alloy. 2024: the high-strength 2xxx example, used when fatigue resistance drives the design. 7075: the highest-strength 7xxx example. On a drawing, these four alloy numbers look interchangeable. On the press floor, they behave very differently. The gap only becomes clear when you put strength and extrudability side b...
Read More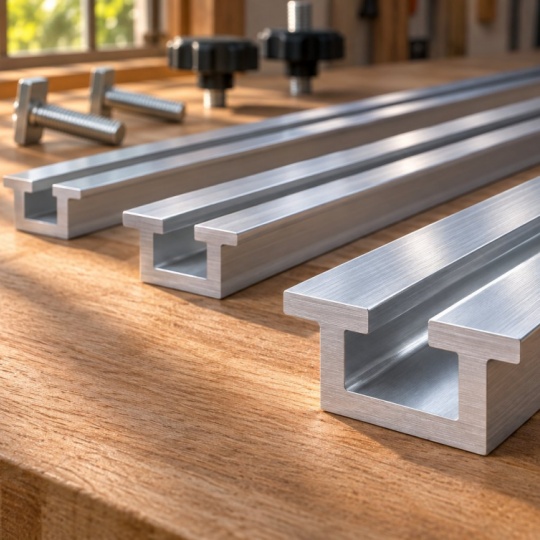
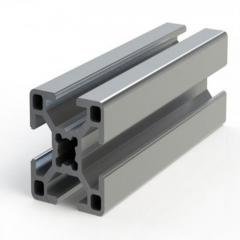
Aluminium T Track Extrusions: What Most Buyers Learn Too Late What Aluminium T-Track Extrusions Are and How They Work Aluminium T-track extrusions are aluminum profiles with one or more T-shaped slots running their full length. You slide a T-bolt, T-nut, or other sliding hardware into the slot, move it to any position, and tighten it to lock a fence, clamp, bracket, or panel in place. The slot has a narrow opening at the surface and a wider cavity underneath. The narrow opening keeps the fastener head from pulling out, and the wider cavity lets it slide freely until you clamp it down. If you have ever moved a fence on a router table and locked it in place without drilling a new hole, you have used this slot. Plain rectangular tubing and basic channel stock only give you flat walls to drill through. A T-track gives you a mounting point along its whole length. Defining the T-Track Profile A slim aluminum t track set into a workbench and the square t slotted aluminum extrusions used in machine frames have the same basic parts: Slot opening: The narrow gap at the surface. Its width decides which bolt shank fits through and which hardware series the profile accepts. Cavity: The wider channel inside, where the T-nut or bolt head rides. Its width and depth decide whether hardware slides smoothly or binds. Flanges: The lips on each side of the opening that hang over the cavity. When you tighten the fastener, the head clamps up against these lips. Web: The back wall that ties the sides together and usually sits against the mounting surface. Wall thickness: How much metal surrounds the slot. Thicker walls resist bending and can take higher clamping force. The overall shape ranges from a low, single-channel track to square sections with a slot on every face. The dimensions are held to tight limits. Xometry notes that T-slot profiles usually follow Aluminum Association standards, with tolerances of about +/- 0.005 to +/- 0.015 inches depending on profile size. How T-Track Differs From Standard Aluminium Channels A U-channel is a flat base with two legs. A C-channel adds lips to the ends of those legs for extra stiffness. Both are useful aluminum extrusions, but neither is designed to hold a fastener head captive while it slides. To mount something, you drill a hole. To move it, you drill another one. A T-slot holds the fastener head, so you can skip the drilling. Hardware goes where you need it today and moves when the job changes tomorrow. That flexibility is why extruded aluminum framing shows up in everything from industrial machine frames to woodworking jig tables. It also makes the profile unforgiving. If the slot is off by a fraction of a millimeter, hardware either binds or wobbles. Catalogs from framing brands and custom extruders such as BRT Extrusions Inc may list the same nominal slot sizes, but the real fit depends on how each aluminum extrusion was made, starting with the steel die that shapes it. How Aluminium T-Track Profiles Are Manufactured ...
Read More


 online service
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 English
 français
 Deutsch
 русский
 español
 português
 العربية
 ไทย
 Việt
 Українська