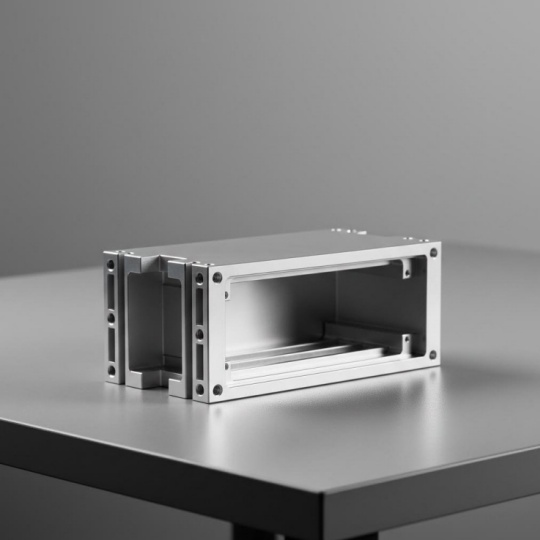
Aluminum Extrusion Electronic Enclosure Secrets: EMI Shielding To IP Ratings What Makes Aluminum Extrusion the Preferred Method for Electronic Enclosures When you're designing housing for sensitive electronic components, the manufacturing method you choose matters just as much as the material itself. An aluminum extrusion electronic enclosure offers something unique: a seamless protective shell created through a continuous forming process that delivers remarkable consistency. But what exactly happens during this process, and why does it outperform alternatives like die-casting or sheet metal fabrication? The Extrusion Process Explained Imagine squeezing toothpaste from a tube—that's essentially how manufacturers extrude aluminum to create enclosures. The process begins with a cylindrical aluminum billet, typically heated to around 400-500°C. At this temperature, the metal becomes malleable without melting completely. A hydraulic ram then applies immense pressure—sometimes up to 15,000 tons—forcing the heated aluminum through a specially designed steel die. The die determines the final cross-sectional shape of your enclosure. As the aluminum passes through, it emerges with a perfectly uniform profile that maintains identical dimensions along its entire length. This is where the magic happens for electronics applications. Unlike die-casting, which involves pouring molten metal into molds and can create internal porosity, the extrusion method produces solid, dense material throughout. After exiting the press, the newly formed profile undergoes rapid cooling through fans or water baths—a step called quenching. This locks in the shape and prepares the material for straightening. Each profile is then stretched to meet precise dimensional standards before being cut to the required lengths. The result? A consistent, high-quality extruded aluminum enclosure ready for secondary operations like machining and finishing. Why Electronics Manufacturers Choose Extruded Profiles So why do engineers consistently choose this method when they need to protect circuit boards, power supplies, and sensitive instrumentation? The answer lies in what the continuous extrusion process delivers that other methods simply cannot match. When you compare an extruded aluminium enclosure to sheet metal alternatives, the difference becomes clear immediately. Sheet metal enclosures require bending, welding, and joining—each connection point represents a potential weakness. In contrast, when manufacturers extrude aluminum through a die, they create a seamless shell with no joints along the primary structure. This seamless construction is critical for electronic component protection because it eliminates potential entry points for dust, moisture, and electromagnetic interference. The uniform wall thickness achieved through extrusion also plays a crucial role. Every section of your aluminum extrusion enclosure maintains identical thermal properties, ensuring consistent heat dissipation ...
Read More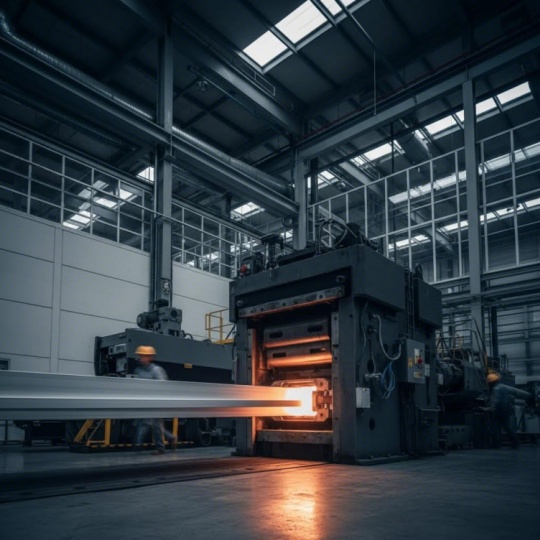
Short Run Aluminum Extrusions: From Custom Die To Delivery What Are Short Run Aluminum Extrusions and When Do You Need Them Ever wondered how companies create custom aluminum extrusion profiles without committing to massive production volumes? The answer lies in short run aluminum extrusions - a manufacturing approach that bridges the gap between one-off prototypes and full-scale mass production. Yet despite its growing importance, the industry rarely defines what "short run" actually means in concrete terms. Short run aluminum extrusions refer to custom-manufactured aluminum profiles produced in limited quantities, typically ranging from 1 to 5,000 pieces, using customer-specific dies and tooling designed for lower-volume production economics. Defining Short Run Quantities in Aluminum Extrusion When you're exploring custom aluminum extrusions, understanding quantity classifications helps you communicate effectively with suppliers and budget accurately for your project. The industry generally recognizes these distinct production tiers: True short runs (1-500 pieces): Ideal for specialized equipment, small aluminum extrusions for niche applications, and market testing scenarios Low-volume production (500-5,000 pieces): Suitable for established products with limited demand or bespoke aluminium extrusion requirements Medium production (5,000-25,000 pieces): Transitional volumes where per-piece costs begin dropping significantly Mass production (25,000+ pieces): Full-scale manufacturing with optimized tooling investments These ranges aren't arbitrary - they reflect real economic thresholds where tooling costs, setup expenses, and material minimums create natural breakpoints in pricing and production strategies. How Short Runs Differ from Prototypes and Mass Production Imagine you've developed a new product design. You might first create prototype aluminum extrusions - perhaps just 5 to 20 pieces - to validate your concept and test functionality. These prototypes often use simplified tooling or even machined samples rather than true extrusion dies. Short run production represents the next phase. You've validated your design and now need enough units for pilot programs, initial customer shipments, or specialized applications. Unlike prototyping, this stage uses production-grade dies capable of delivering consistent aluminum extrusion profiles across every piece. The key characteristics that define short run extrusion projects include: Custom die development with careful cost-benefit analysis Production-quality tooling designed for reusability Full material traceability and quality certification Access to secondary operations like machining and finishing Flexible scheduling without long-term volume commitments This manufacturing approach has become increasingly vital for product development cycles, custom applications in specialized industries, and companies seeking to minimize inventory while maintaining supply flexibility. Whether you're developing me...
Read More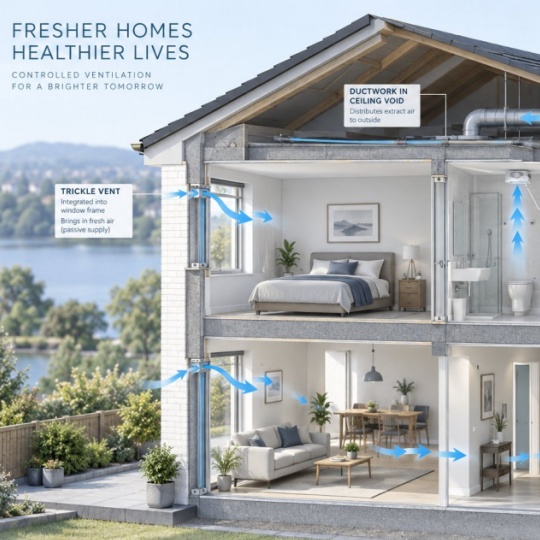
UK Building Regulations Ventilation Decoded: From Part F to Sign-Off What UK Building Regulations Require for Ventilation Every building in the United Kingdom, whether a single-bedroom flat or a multi-storey office block, must provide adequate ventilation to protect the health of its occupants. That obligation is not optional guidance or best practice. It is law. UK building regulations ventilation requirements mandate that fresh air enters a building, stale air is extracted, and indoor pollutants like moisture, carbon dioxide, and volatile organic compounds never accumulate to harmful levels. UK building regulations require that buildings are provided with adequate means of ventilation to supply fresh outdoor air, limit the concentration of indoor pollutants harmful to health, and control excess moisture that could lead to condensation and mould growth. In England, this is set out in Part F of Schedule 1 to the Building Regulations 2010, supported by statutory guidance in Approved Document F. Sounds straightforward? In practice, ventilation compliance touches multiple regulatory documents, differs across England, Scotland, Wales, and Northern Ireland, and creates real design tensions with energy efficiency and fire safety rules. This guide breaks it all down, reproducing the actual data professionals need so you never have to dig through 100-page government PDFs again. The Legal Foundation Behind Ventilation Requirements The entire regulatory framework flows from a single piece of primary legislation: the Building Act 1984. This Act gives the Secretary of State power to make building regulations for England and Wales, covering the health, safety, welfare, and convenience of building occupants. The Building Regulations 2010, made under that Act, set out the functional requirements that all building work must satisfy. Schedule 1 of these Regulations organises those requirements into lettered "Parts," each covering a specific aspect of building performance. Part F deals specifically with ventilation. Its requirement is deliberately broad: there shall be adequate means of ventilation provided for people in a building. The detail of how to actually meet that requirement lives in the Approved Documents. These are not law themselves, but they carry significant statutory weight. If you follow the guidance in an Approved Document, you are treated as having complied with the relevant regulation. Deviate from it, and the burden falls on you to demonstrate that your alternative approach achieves at least the same standard. Think of it as a hierarchy. The Building Act 1984 sits at the top, establishing the legal authority. The Building Regulations 2010 translate that authority into enforceable functional requirements. The Approved Documents then provide the practical, technical roadmap for meeting those requirements on site. Why Ventilation Is a Regulatory Priority Why does the government regulate something as seemingly simple as airflow? Because the consequ...
Read More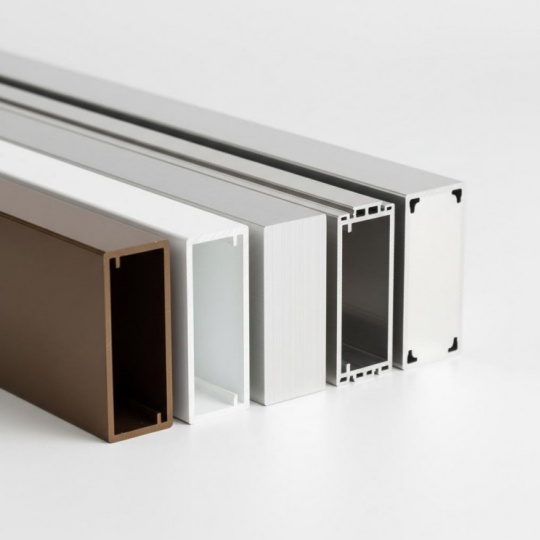
Finishing Services For Aluminum Extrusions: Match Your Alloy To The Right Method Understanding Finishing Services for Aluminum Extrusions When you picture aluminum extrusion profiles coming off the production line, you might assume they're ready for immediate use. After all, aluminum is naturally corrosion-resistant, right? While that's partially true, raw extruded aluminum profiles rarely go directly into their final applications. Instead, they undergo finishing services for aluminum extrusions—a collection of surface treatments that transform basic aluminum shapes into components ready for demanding real-world environments. These finishing processes aren't optional upgrades. They're essential steps that determine how well your aluminum profiles will perform over years of service. Whether you're working with standard aluminum shapes or curved aluminum extrusion designs, the right finish makes the difference between components that thrive and those that fail prematurely. Why Raw Aluminum Needs Surface Treatment Here's something that might surprise you: aluminum does form a natural protective oxide layer when exposed to air. This thin film offers some baseline corrosion resistance, which is why aluminum doesn't rust like steel. However, this natural barrier is extremely thin—only about 2 to 3 nanometers—and provides minimal protection against mechanical wear, chemical exposure, or harsh environmental conditions. Think about where extruded aluminum profiles actually end up. Architectural facades face decades of UV exposure and weather cycling. Marine components encounter salt spray daily. Industrial equipment endures constant abrasion and chemical contact. In each case, that microscopic natural oxide layer simply isn't enough. Proper finishing treatments can extend aluminum component lifespan by 3 to 10 times compared to untreated surfaces, depending on the application environment and selected finish type. Beyond protection, there's another practical consideration. Raw aluminum has a somewhat dull, industrial appearance that doesn't meet aesthetic requirements for consumer products, architectural elements, or visible components. Surface treatments solve both problems simultaneously. The Dual Purpose of Finishing - Protection and Aesthetics Finishing services for aluminum extrusions serve two interconnected purposes that manufacturers must balance based on their specific application needs: Functional Protection: This includes enhanced corrosion resistance through thickened oxide layers or protective coatings, improved wear resistance for components facing mechanical stress, and thermal or electrical properties modification. According to industry expertise from Rapid Axis, treatments like anodizing create durable barriers against moisture, chemicals, and salt spray—critical for aerospace, electronics, and architectural applications. Aesthetic Enhancement: Surface treatments enable color customization ranging from subtle metallic tones to vibrant hues...
Read More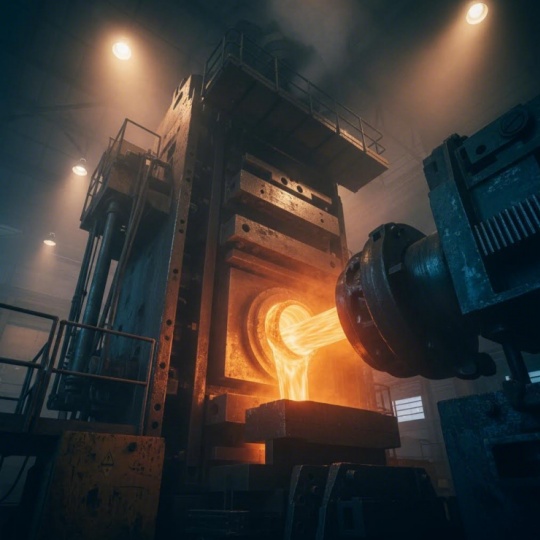
Hollow Aluminum Extrusion Secrets: Die Types Your Supplier Won't Explain What Is Hollow Aluminum Extrusion and Why It Matters When you need structural components that deliver strength without unnecessary weight, understanding hollow aluminum extrusion becomes essential. This manufacturing process transforms heated aluminum billets into profiles with internal cavities - creating everything from simple round tubes to complex multi-void industrial sections. Hollow aluminum extrusion is a manufacturing process where pre-heated aluminum billets are forced through specialized tooling containing mandrels and bridges, allowing the metal to flow around internal supports and weld back together to form profiles with enclosed void spaces. Unlike simpler solid extrusion methods, creating hollow profiles requires the aluminum to split, flow around mandrel supports, then rejoin seamlessly in a welding chamber before exiting the die. This sophisticated process enables manufacturers to produce hollow aluminum rods, tubes, and complex alu profile shapes that would be impossible to achieve otherwise. What Makes Hollow Extrusions Different from Solid Profiles Imagine squeezing play-dough through a shaped opening - that's essentially how solid extrusions work. Hollow profiles, however, demand far more complex engineering. The tooling must incorporate mandrels that define internal voids while bridges or legs provide structural support to withstand pressures that can reach up to 15,000 tons during the extrusion process. The fundamental difference lies in structural efficiency. Solid aluminum sections contain more material in their cross-section, providing excellent compressive strength. However, hollow profiles consist of hollow tubes which provide support through their outer walls carrying most of the load. This engineering principle delivers remarkable weight-to-strength ratios that solid profiles simply cannot match. Consider this practical comparison: a hollow tubular beam can offer equivalent bending and torsional resistance to a solid bar while using significantly less material. This translates directly to lighter components, reduced material costs, and easier handling during installation. The Core Mechanics Behind Hollow Profile Creation The physics behind hollow extrusion centers on controlled metal flow and precise rejoining. When aluminum enters the die, it encounters mandrel supports (called legs or bridges) that split the material stream. The separated aluminum flows around these supports, then converges in the welding chamber where temperature and pressure conditions force the metal streams to fuse into a continuous, seamless shell. This rejoining process is critical. If the tooling design or process parameters are incorrect, weak weld lines form where the metal streams meet - or worse, the internal cavity may collapse entirely. Successful hollow extrusion depends on: Proper billet heating to ensure optimal material flow Precisely engineered mandrel and br...
Read More


 online service
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 English
 français
 Deutsch
 русский
 español
 português
 العربية
 ไทย
 Việt
 Українська